Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
Precision-engineered conical drums purpose-built for new energy enterprises handling lithium battery electrolytes and hazardous solvents.
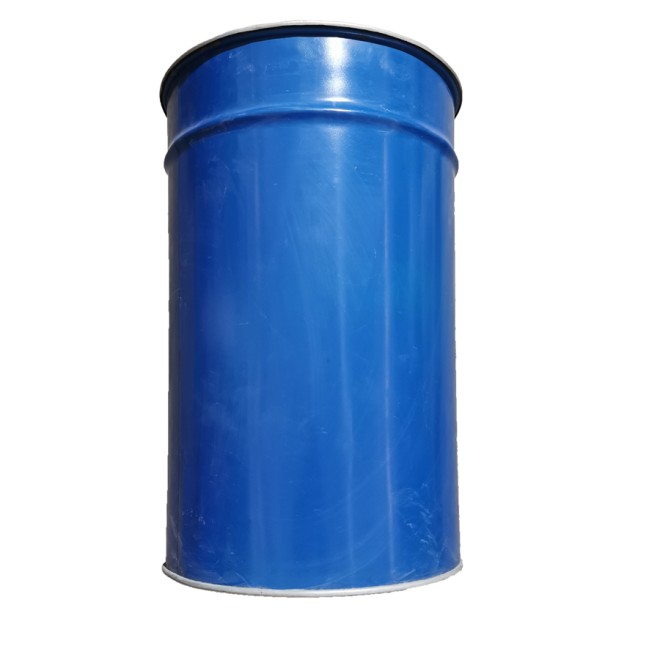
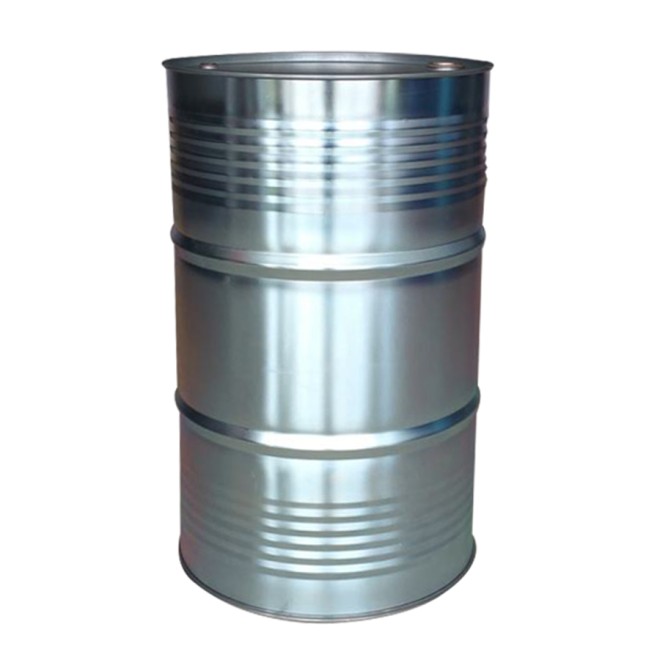
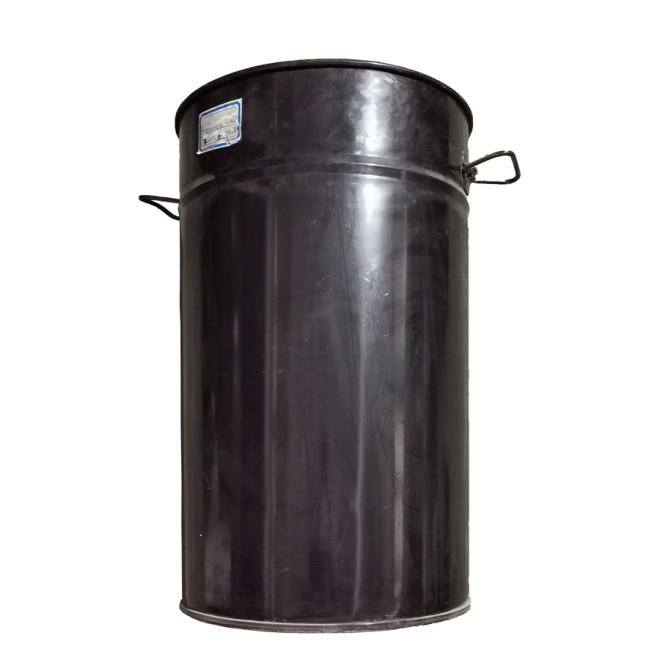
Understanding the industrial landscape that is driving unprecedented demand for certified, high-performance conical drum packaging.
The global new energy sector — encompassing electric vehicles (EVs), grid-scale energy storage systems (ESS), and consumer electronics — has entered an era of exponential growth. According to industry forecasts, global lithium-ion battery production capacity is projected to exceed 5,500 GWh annually by 2030, with the Asia-Pacific region, particularly China, South Korea, and Japan, accounting for the dominant share. This explosive growth directly translates into massive, sustained demand for safe, reliable, and regulation-compliant packaging solutions for the hazardous chemical inputs that power these batteries.
At the heart of every lithium-ion battery lies a carefully formulated electrolyte — typically a lithium salt dissolved in organic carbonate solvents such as ethylene carbonate (EC), dimethyl carbonate (DMC), diethyl carbonate (DEC), and ethyl methyl carbonate (EMC). These solvents are classified as hazardous materials under international regulations including the UN Model Regulations, IATA DGR, IMDG Code, and ADR/RID. They are flammable, moisture-sensitive, and chemically aggressive — demanding packaging that provides an absolute barrier against leakage, contamination, and environmental exposure throughout the entire supply chain.
A single packaging failure during the transport of lithium battery electrolytes can trigger regulatory shutdowns, environmental liability, and catastrophic safety incidents. For new energy enterprises, selecting certified, purpose-engineered conical drums is not a procurement decision — it is a fundamental risk management imperative that protects supply chains, personnel, and brand reputation.
The conical drum — characterised by its tapered body geometry — has emerged as the preferred packaging format for high-value, hazardous battery solvents for several compelling engineering reasons. The conical shape enables near-complete product drainage, which is critical when handling expensive electrolyte formulations where residual waste represents significant financial loss. The geometry also provides superior stacking stability during pallet transport and warehouse storage, reducing the risk of toppling and accidental damage.
Furthermore, conical drums can be nested when empty, dramatically reducing return logistics costs and storage footprint — a significant operational advantage for large-scale battery manufacturers who cycle thousands of drums per month. When combined with high-performance interior linings such as epoxy coatings or stainless steel construction, conical drums deliver the chemical resistance, purity preservation, and mechanical integrity that the new energy supply chain demands.
Solvent conical drums serve multiple critical nodes across the battery manufacturing and energy storage supply chain.
Lithium hexafluorophosphate (LiPF₆) and carbonate solvent blends require UN-certified, chemically inert packaging. Epoxy-lined conical drums prevent ionic contamination and maintain electrolyte purity from chemical plant to battery cell manufacturer — a journey that may cross multiple international borders.
Inside modern EV battery gigafactories, conical drums serve as the primary intermediate bulk container for solvent distribution across electrode coating lines, electrolyte filling stations, and formation cycling areas. The nesting capability of conical drums is particularly valued in space-constrained cleanroom environments.
The rapidly growing battery recycling industry requires robust containment for recovered solvents, black mass slurries, and intermediate processing chemicals. Stainless steel conical drums provide the chemical resistance and cleanability needed for circular economy operations where contamination cross-over must be strictly controlled.
Chemical exporters supplying battery-grade solvents to overseas gigafactories must comply with IMDG Code (sea freight), IATA DGR (air freight), and ADR (road transport) regulations simultaneously. Our conical drums carry the necessary UN type approvals to satisfy multi-modal transport requirements across all major shipping routes.
Utility-scale ESS deployments require enormous volumes of electrolyte, delivered on tight construction schedules. Large-format 200-230L conical drums optimise palletisation density and minimise handling operations at remote project sites, where logistics efficiency is critical and re-supply is costly.
Battery research institutes and pilot production facilities require smaller-format conical drums (10L–60L) for handling experimental electrolyte formulations, novel solvent systems, and additive packages. The precise drainage characteristics of conical drums are essential for accurate material accounting in R&D environments.
Four macro-trends are reshaping the requirements for hazardous battery material packaging through 2030 and beyond.
Regulatory bodies worldwide are continuously updating UN Model Regulations, ADR, IMDG, and national standards to address the unique hazard profiles of next-generation battery chemistries including sodium-ion, solid-state, and lithium-sulfur systems. Packaging manufacturers must invest in ongoing certification programmes to maintain compliance across evolving regulatory landscapes.
New energy enterprises are under intense ESG pressure to minimise packaging waste. Returnable, refurbishable conical drum programmes — enabled by the drums' durability and nesting capability — are gaining traction as alternatives to single-use packaging, reducing both carbon footprint and total cost of ownership for high-frequency battery material supply chains.
As battery chemistries advance toward higher energy density and faster charging, electrolyte formulations are becoming increasingly complex — incorporating multiple solvents, lithium salts, and functional additives. This complexity demands packaging with superior chemical inertness, moisture exclusion, and contamination prevention to protect formulation integrity during extended supply chain transit times.
Geopolitical pressures and supply chain resilience strategies are driving battery manufacturers to regionalise their electrolyte supply chains. This trend increases the demand for locally-sourced, certified packaging solutions that can be rapidly scaled to meet the surge demands of new gigafactory openings in Europe, North America, and Southeast Asia.
When specifying conical drums for hazardous battery solvent applications, procurement engineers and safety managers should evaluate several critical technical parameters. Interior lining compatibility is paramount — epoxy phenolic linings provide excellent resistance to carbonate solvents, while stainless steel (316L grade preferred) offers the highest level of chemical inertness for ultra-high-purity applications. Closure integrity must be verified against the specific vapour pressure and temperature range of the transported material, with UN-certified bungs and seals rated for the relevant packing group.
Wall thickness and structural integrity must withstand the mechanical stresses of palletised transport, including forklift handling, vibration during road and sea transit, and stacking loads in warehouse storage. For international shipments, the drum must carry appropriate UN markings specifying the design type code, packing group rating, maximum gross mass, and year of manufacture — all of which must be verified against the relevant transport regulations for the specific route and mode.
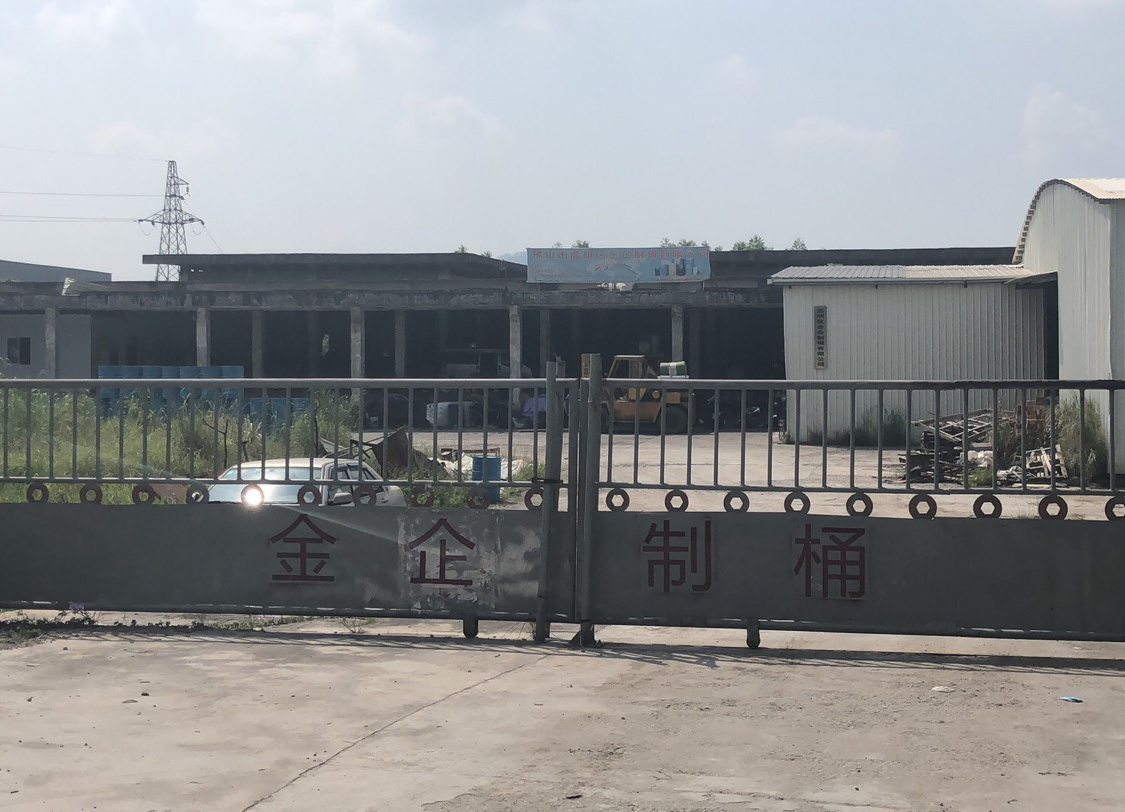
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007 (formerly known as Nanzhuang Ironworks Metal Products Factory). It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning. We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.
With over two decades of specialised manufacturing experience, we have developed deep expertise in producing conical drums that meet the exacting standards required by new energy enterprises, chemical distributors, and hazardous goods logistics providers across global markets. Our production capabilities span a full range of volumes, materials, and surface treatments to address every node of the battery material supply chain.
The values that underpin every drum we manufacture and every partnership we build.

We pledge to deliver within agreed deadlines, meet specified standards, and stand by our commitment with our company's reputation as guarantee.

We strive to exceed customer expectations, producing products worthy of their trust — especially critical for hazardous battery material containment.

We offer competitive pricing to serve our broad customer base, making certified hazardous goods packaging accessible at scale.

We prioritise client requirements, tailoring our production to meet their specifications — from custom linings to bespoke volume configurations.
Our quality management systems and product certifications validate our commitment to manufacturing excellence and regulatory compliance.
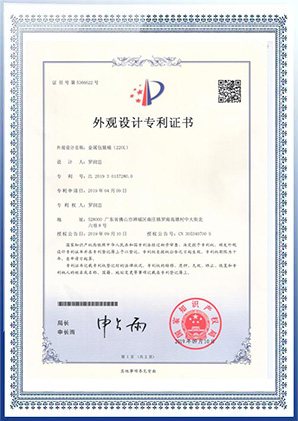
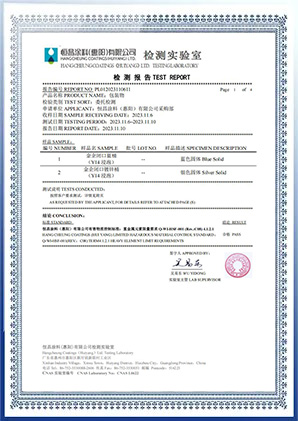
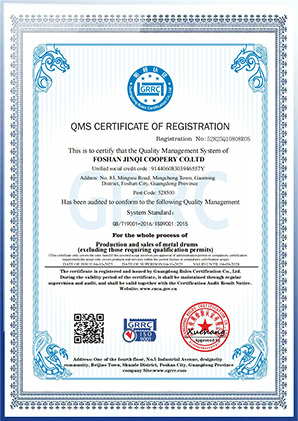
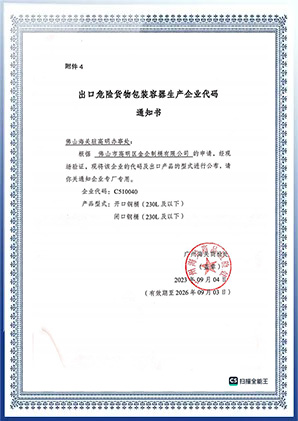
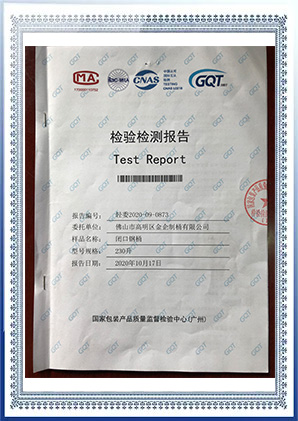
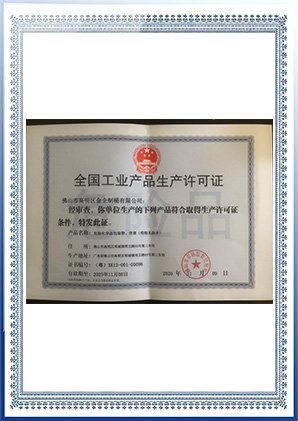
Our full portfolio of certified steel drums and conical containers for new energy enterprise logistics — engineered for safety, compliance, and operational efficiency.
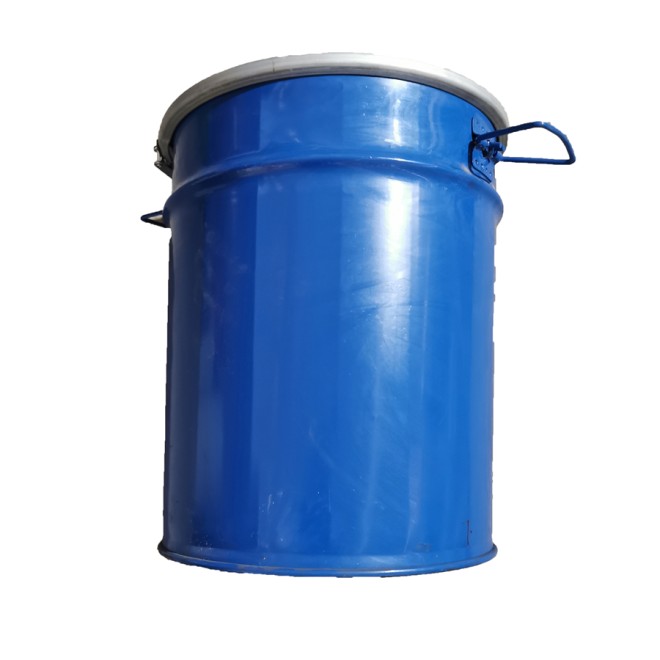
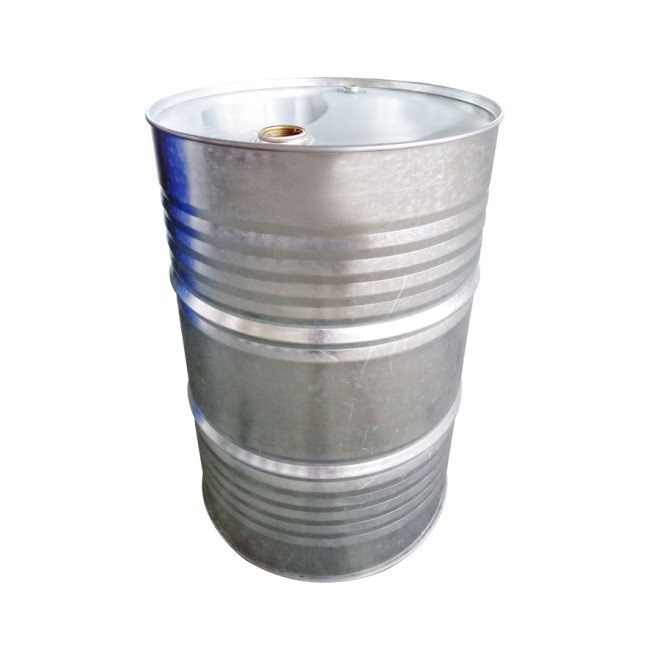
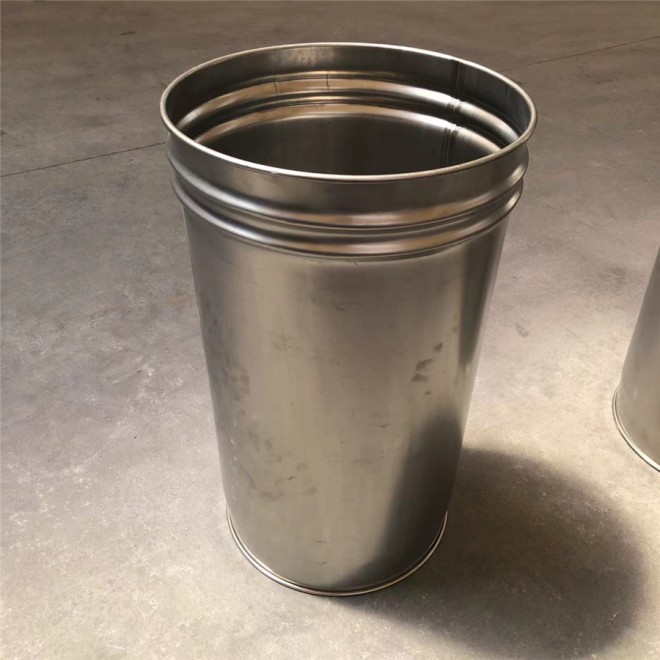
Whether you operate a gigafactory, manage chemical distribution for new energy supply chains, or require compliant packaging for international hazardous goods transport — our engineering team is ready to deliver the right conical drum solution for your application.
Request a Consultation