Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
Explore our top-rated containment products engineered for sterile liquid ingredients in pharmaceutical environments.
In the highly regulated world of pharmaceutical manufacturing, the integrity of every container used to store, transport, or process sterile liquid ingredients is not merely a logistical concern — it is a patient safety imperative. Resin closed head steel drums have emerged as the gold standard for pharmaceutical companies that demand absolute containment reliability, chemical resistance, and compliance with international regulatory frameworks such as FDA 21 CFR, EU GMP Annex 1, and ICH Q7 guidelines.
A resin closed head steel drum combines the structural strength of high-grade steel with an interior resin lining — typically epoxy phenolic, polyethylene, or fluoropolymer-based — that creates an inert, non-reactive barrier between the container wall and the liquid contents. This dual-material construction is critical when handling APIs (Active Pharmaceutical Ingredients), excipients, sterile water for injection (WFI), biological buffers, solvent-based formulations, and other sensitive liquid ingredients where even trace contamination can compromise product efficacy or patient safety.
Resin closed head steel drums provide a hermetically sealed, pressure-tested containment environment that prevents microbial ingress, oxidation, and cross-contamination — making them indispensable across vaccine production, biologics manufacturing, sterile injectable preparation, and advanced drug formulation facilities worldwide.
The global pharmaceutical packaging market is projected to exceed USD 175 billion by 2030, driven by surging demand for biologics, gene therapies, and sterile injectable drugs. Within this landscape, industrial-grade drum packaging — particularly resin-lined closed head steel drums in capacities ranging from 10L to 230L — plays a pivotal role in the cold chain, bulk ingredient logistics, and cleanroom supply operations of pharmaceutical plants worldwide.
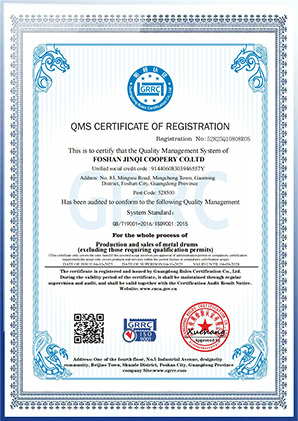
Pharmaceutical manufacturers face increasing pressure from regulatory authorities to demonstrate container-closure integrity (CCI) at every stage of the supply chain. Resin closed head steel drums, when manufactured to UN/DOT standards and validated under ISO 9001 quality management systems, provide the documented traceability and test certification that regulatory auditors require. Their robust steel construction withstands the rigors of international freight — including stacking loads, temperature cycling, and humidity fluctuations — while the sealed resin interior maintains sterility throughout transit.
Asia-Pacific, led by China, India, and South Korea, has become the world's largest manufacturing hub for pharmaceutical-grade steel drums. Chinese manufacturers such as Foshan Qiaoyue Packaging Co., Ltd. have invested heavily in automated production lines, precision welding technology, and advanced resin application systems to meet the exacting demands of global pharmaceutical clients. The competitive advantage of Chinese-manufactured resin closed head steel drums lies in their combination of cost-efficiency, customization flexibility, and increasingly rigorous quality certifications.
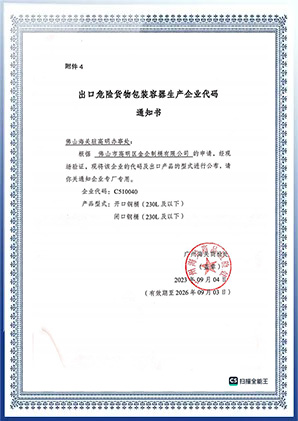
Major pharmaceutical companies — including contract manufacturers (CMOs) and contract development and manufacturing organizations (CDMOs) — are consolidating their approved supplier lists, favoring drum manufacturers who can demonstrate ISO certification, UN approval for hazardous material transport, and the ability to produce pharmaceutical-grade drums with full batch traceability documentation. This shift is driving mid-tier drum manufacturers to upgrade their quality systems and invest in cleaner production environments.
Engineered to meet the strictest pharmaceutical containment and regulatory standards worldwide.
The closed head design with gasket-sealed bungs and plugs ensures zero leakage under pressure, maintaining sterile conditions throughout storage and transport of sensitive pharmaceutical liquids.
Interior epoxy phenolic or polyethylene resin coatings provide complete chemical inertness, preventing metal ion migration, corrosion, and contamination of sterile liquid ingredients including APIs and biologics.
Manufactured to UN/DOT, FDA, EU GMP, and ISO 9001 standards with full documentation support for regulatory submissions, batch traceability, and container-closure integrity validation.
High-grade steel construction withstands extreme temperature ranges from cold chain logistics (-20°C) to autoclave sterilization cycles, maintaining structural integrity and seal performance throughout.
Steel drums offer superior recyclability compared to plastic alternatives, supporting pharmaceutical companies' ESG commitments and circular economy initiatives without compromising containment performance.
Available in capacities from 10L to 230L with customizable resin formulations, coating thicknesses, bung configurations, surface treatments, and labeling to meet specific pharmaceutical process requirements.
The intersection of pharmaceutical innovation and industrial packaging is driving significant evolution in resin closed head steel drum technology.
The explosive growth of biologics, monoclonal antibodies, and emerging cell and gene therapies requires containment solutions with ultra-low extractables and leachables profiles. Next-generation resin formulations — including fluoropolymer-lined steel drums — are being developed specifically for these high-value, highly sensitive liquid ingredients, where even sub-ppm contamination levels can invalidate entire production batches.
Post-pandemic pharmaceutical supply chain disruptions have accelerated the diversification of approved packaging suppliers across multiple geographies. Pharmaceutical companies are qualifying additional drum suppliers in Asia and establishing regional inventory buffers, creating new market opportunities for certified manufacturers capable of meeting GMP documentation requirements and rapid delivery timelines.
Leading drum manufacturers are integrating automated resin application systems, robotic welding, and inline vision inspection technologies to achieve consistent coating thickness, weld integrity, and surface quality that manual processes cannot reliably deliver. RFID-enabled drum tracking and digital batch records are emerging as standard requirements for pharmaceutical supply chain transparency.
Regulatory and corporate ESG pressures are driving the transition from solvent-based resin coatings to water-based and UV-cured alternatives that reduce VOC emissions and worker exposure. Steel drum manufacturers are also adopting closed-loop water recycling, energy-efficient curing ovens, and responsible chemical sourcing to align with pharmaceutical customers' sustainability reporting requirements.
Convergence of FDA, EMA, ICH, and WHO packaging guidelines is establishing globally consistent standards for pharmaceutical container qualification. Drum manufacturers serving multinational pharmaceutical clients must now maintain multi-jurisdictional regulatory files, conduct extractables and leachables studies, and participate in supplier qualification audits — raising the barrier to entry and rewarding established, certified manufacturers.
Resin closed head steel drums serve critical functions across the full pharmaceutical production lifecycle.
In the production of parenteral drugs — including IV solutions, lyophilized injectables, and pre-filled syringe formulations — bulk sterile liquid ingredients must be transferred and stored in containers that provide absolute microbial exclusion. Resin closed head steel drums with validated CCI (container-closure integrity) serve as the primary bulk holding vessels between synthesis, filtration, and aseptic fill-finish operations, maintaining sterility assurance levels (SAL) of 10⁻⁶ or better.
Active Pharmaceutical Ingredients in liquid form — including solvent-dissolved APIs, liquid excipients such as PEG, polysorbate 80, and benzyl alcohol — require containment that prevents oxidation, moisture ingress, and chemical degradation. Resin-lined steel drums provide the vapor barrier and chemical resistance necessary to maintain API potency and excipient specification compliance during warehousing and inter-facility transport.
Vaccine manufacturing involves the handling of highly sensitive biological materials including cell culture media, adjuvant solutions, stabilizer buffers, and viral antigen suspensions. The ultra-clean interior surfaces of pharmaceutical-grade resin lined steel drums prevent protein adsorption, maintain pH stability, and eliminate the risk of endotoxin contamination that could compromise vaccine immunogenicity and patient safety.
Solvents such as ethanol, isopropanol, acetonitrile, and dichloromethane are widely used in pharmaceutical synthesis, extraction, and purification processes. Resin closed head steel drums rated for flammable liquids (UN Class 3) provide the required combination of electrostatic grounding capability, pressure resistance, and chemical inertness for safe handling, storage, and transport of these hazardous pharmaceutical solvents in compliance with ADR/IATA/IMDG regulations.
CDMOs operating multi-product facilities face complex cross-contamination prevention challenges. Dedicated single-use or validated-for-reuse resin lined steel drums with unique identification coding enable strict campaign separation, cleaning validation documentation, and rapid changeover between different pharmaceutical product campaigns, supporting the flexible manufacturing models that characterize modern CDMO operations.
Temperature-sensitive pharmaceutical liquids — including insulin formulations, blood plasma derivatives, and mRNA vaccine components — require packaging that maintains thermal stability during cold chain distribution. Resin closed head steel drums, when used in conjunction with validated insulated shipping systems, provide the structural rigidity and seal integrity that flexible plastic containers cannot guarantee under the mechanical stresses of international cold chain logistics.
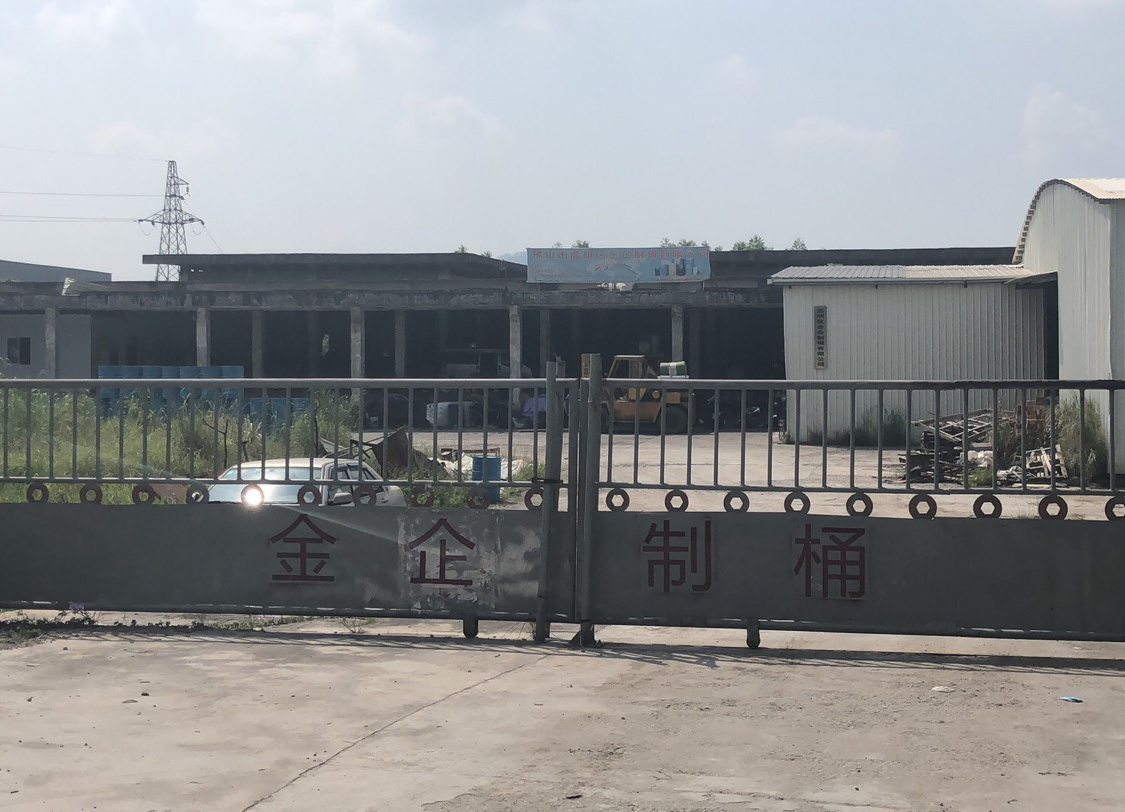
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007 (formerly known as Nanzhuang Ironworks Metal Products Factory). It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning. We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.

We pledge to deliver within agreed deadlines, meet specified standards, and stand by our commitment with our company's reputation as guarantee.

We strive to exceed customer expectations, producing products worthy of their trust.

We offer competitive pricing to serve our broad customer base.

We prioritise client requirements, tailoring our production to meet their specifications.
Partner with Foshan Qiaoyue Packaging for certified, pharmaceutical-grade resin closed head steel drums that meet your regulatory and operational requirements.
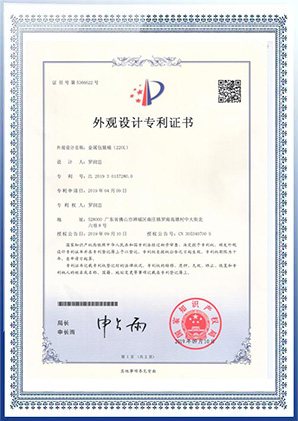
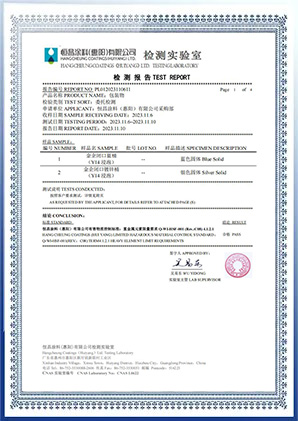
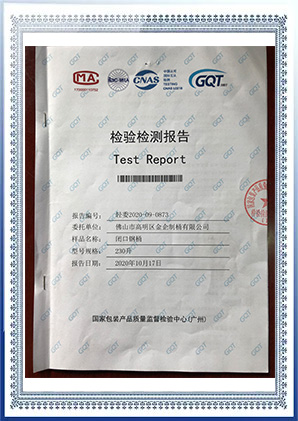
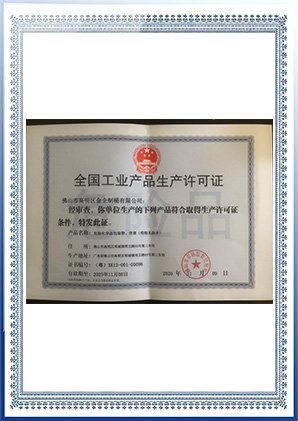
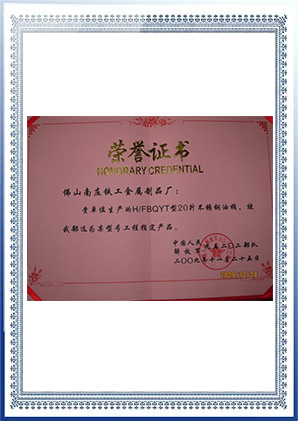
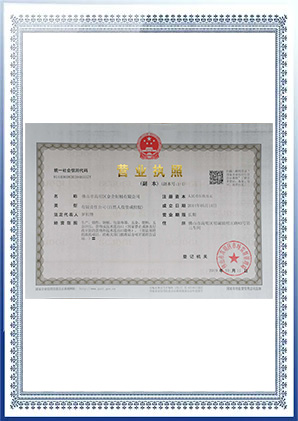
Get Started NowOur quality management systems and product certifications validate our commitment to pharmaceutical-grade manufacturing standards.
Browse our full selection of pharmaceutical-compatible steel drum solutions for sterile liquid ingredient handling and transport.