Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
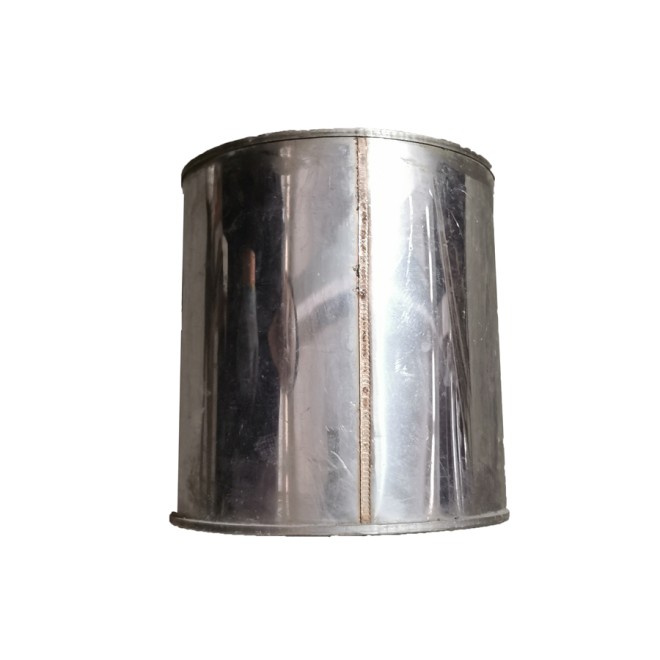
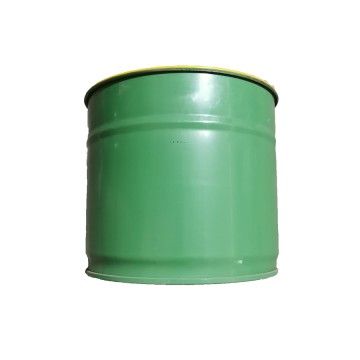
In the modern globalized food industry, transporting bulk ingredients and high-value juice concentrates demands packaging solutions that guarantee absolute purity, chemical stability, and structural durability. The term "Resin Chemical Drum" has evolved beyond traditional chemical storage. Today, it represents a specialized class of high-barrier, food-safe containers engineered with advanced polymer linings and protective resin coatings. These drums serve as the backbone for bulk food ingredient suppliers and juice concentrate exporters who operate across complex, multi-modal international supply chains.
For bulk food ingredient suppliers, maintaining the sensory properties—taste, aroma, color, and texture—of their products is paramount. Traditional raw steel or standard plastic containers often fail to provide the necessary protection against oxidation, chemical migration, and environmental contamination. Resin chemical drums address these issues by combining the mechanical strength of steel with the chemical inertness of high-performance polymer resins. The inner lining, typically composed of epoxy-phenolic resins, creates a robust barrier that prevents any direct contact between the product and the steel shell, eliminating the risk of rust contamination or metal pickup.
Juice concentrate exporters face a unique set of logistical and preservation challenges. Concentrates, especially those derived from citrus fruits, grapes, and berries, are highly acidic and contain natural sugars that are susceptible to fermentation and chemical breakdown under inadequate storage conditions. Here is how advanced resin chemical drums solve these critical pain points:
The industrial packaging sector is undergoing a rapid transformation, driven by regulatory pressures, sustainability mandates, and the need for cost efficiency. Bulk ingredient suppliers are actively seeking packaging that supports circular economy principles without compromising on safety. The latest generation of resin chemical drums incorporates bio-based resin linings and lightweight yet high-tensile steel alloys, reducing the carbon footprint of transport. Additionally, the reusability and recyclability of steel drums make them a preferred choice over single-use plastics, aligning with global corporate sustainability goals.
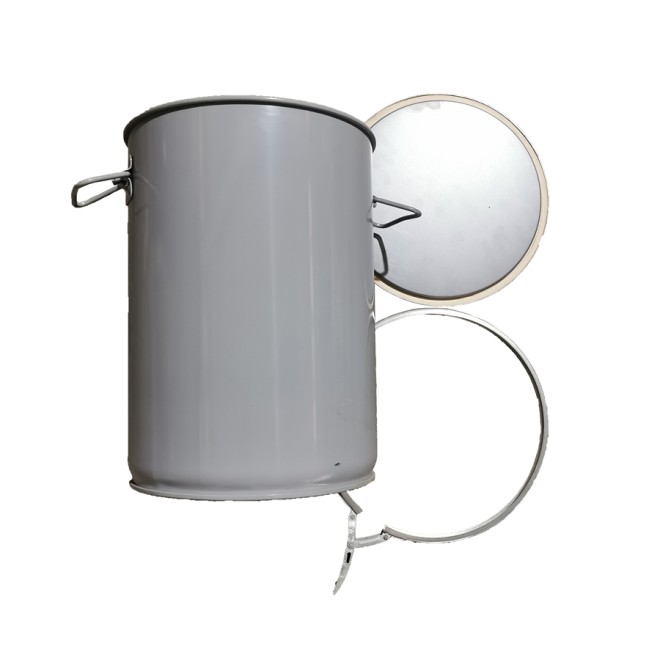
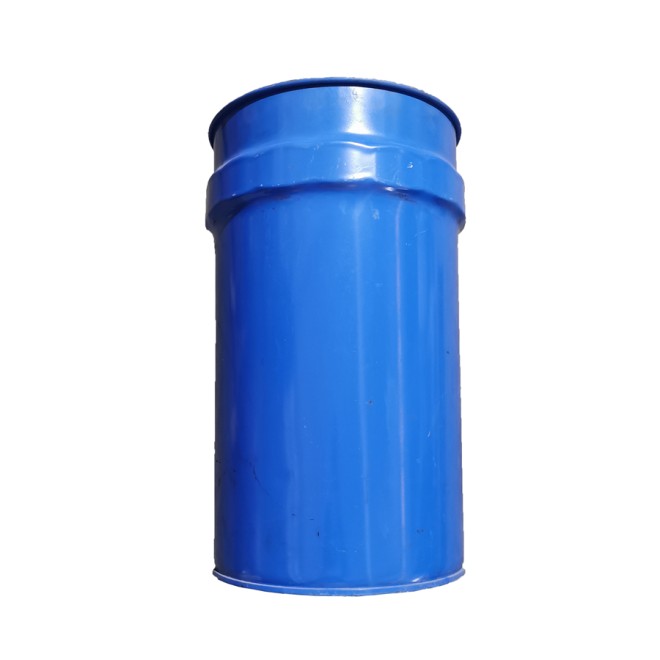
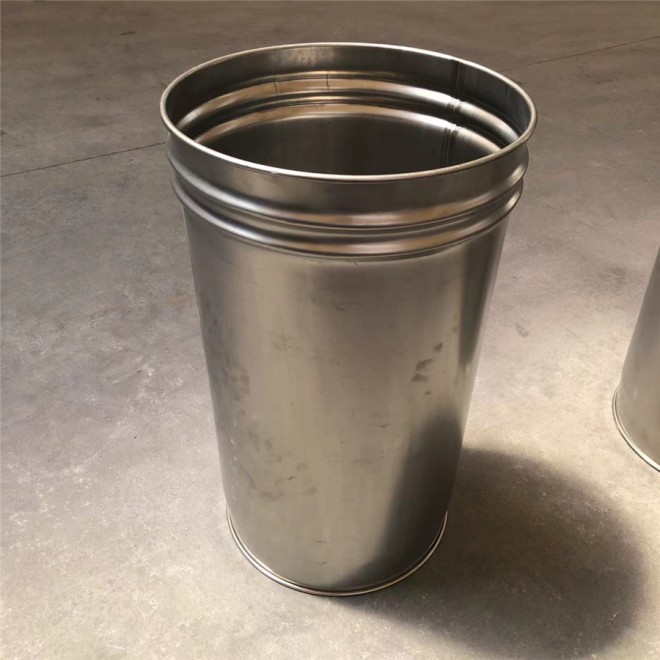
Space optimization is a key driver in reducing shipping costs. Conical resin drums have gained massive popularity among exporters. Unlike traditional cylindrical drums, conical drums can be nested when empty, significantly reducing warehouse storage requirements and lowering return logistics costs. When filled, their structural geometry allows for secure stacking in standard ISO containers, maximizing shipping volume and minimizing movement during transit.
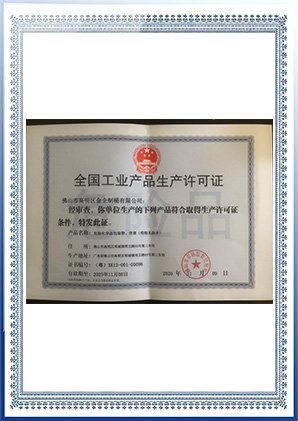
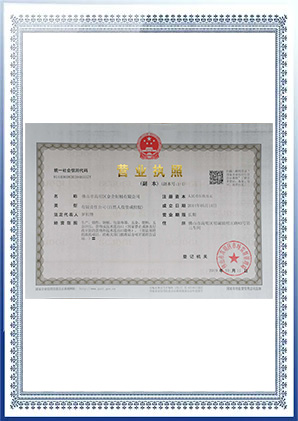
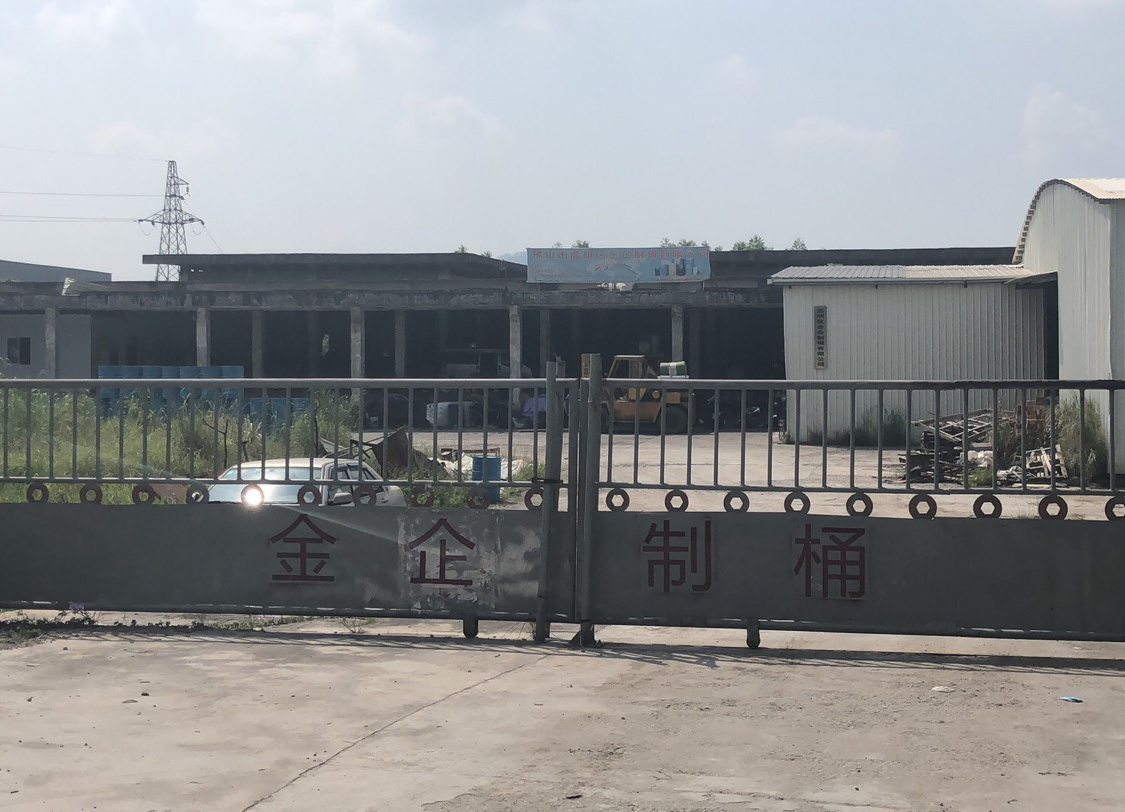
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007 (formerly known as Nanzhuang Ironworks Metal Products Factory). It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning. We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.


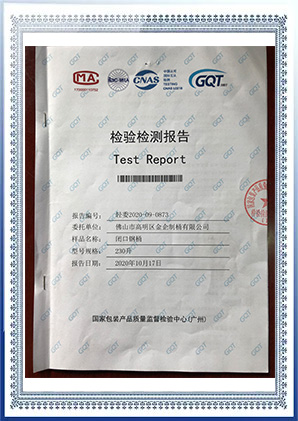
When dealing with bulk food ingredients and juice concentrates, regulatory compliance is non-negotiable. Resin chemical drums used in these sectors must meet rigorous international standards, including the United States Food and Drug Administration (FDA) regulations and the European Union (EU) Regulation No 1935/2004. These regulations ensure that the packaging materials do not transfer their constituents into the food in quantities that could endanger human health, bring about an unacceptable change in the composition of the food, or deteriorate its organoleptic characteristics.
At Foshan Qiaoyue Packaging Co., Ltd., our manufacturing process is meticulously controlled to ensure the highest standards of safety and durability. It begins with the selection of premium cold-rolled steel sheets, which are formed into the drum body. The inner surface is then treated and coated with a specialized food-grade resin lining. This coating is cured at high temperatures to form a cross-linked, impervious barrier. Each drum undergoes strict quality control checks, including leak testing, coating thickness verification, and adhesion tests, ensuring they can withstand the rigors of global export shipping.
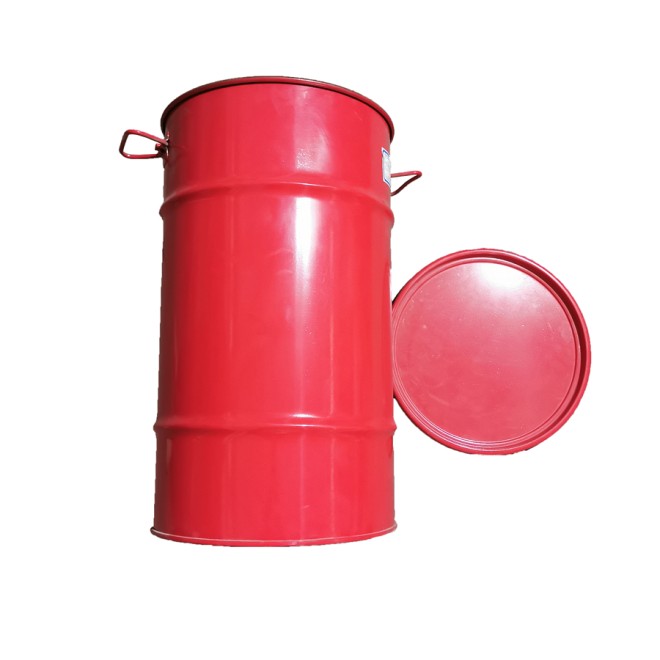
Our commitment to continuous innovation and learning allows us to adapt our products to the changing needs of the market. Whether you require specific handle configurations, custom colors for branding, or specialized coatings for highly aggressive food ingredients, we provide tailored solutions to match your logistics and storage requirements.