Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
Precision-engineered open head steel drums designed for specialty chemical plants — combining UN compliance, corrosion resistance, and superior containment for flammable solvents.
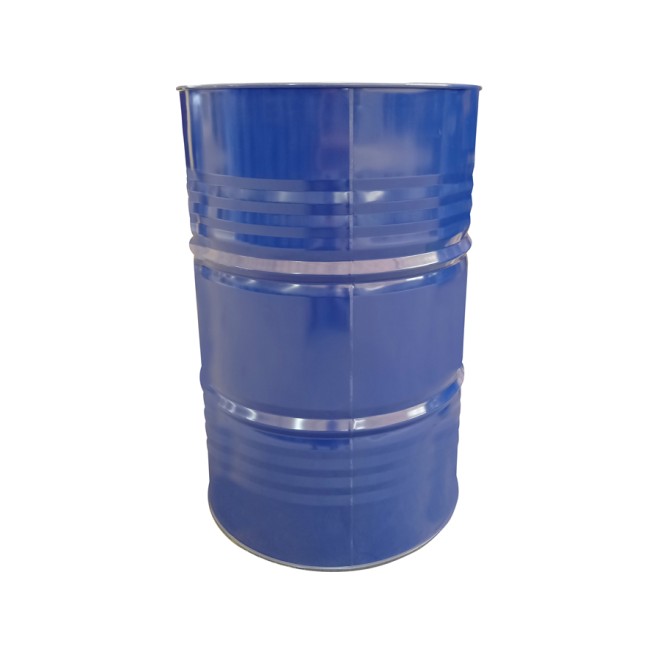
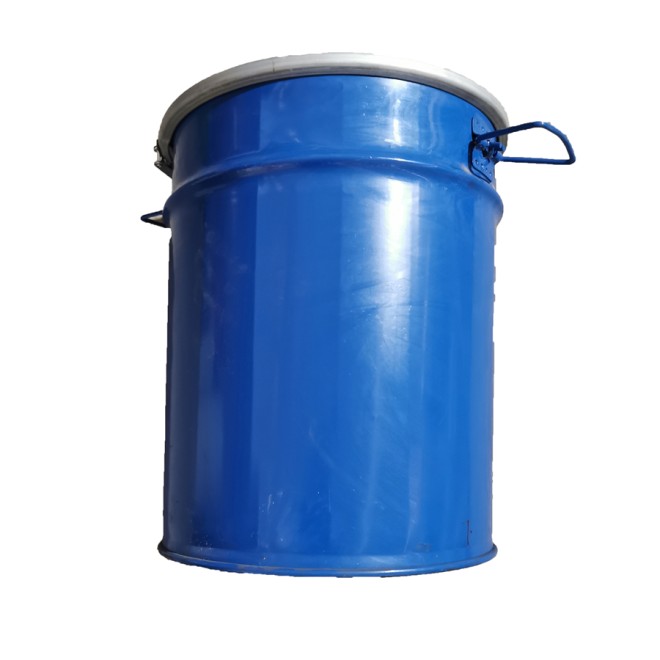
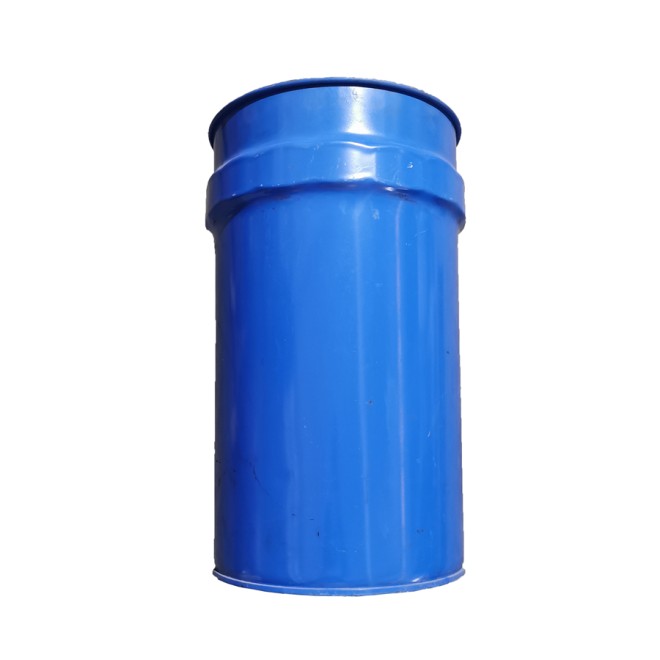
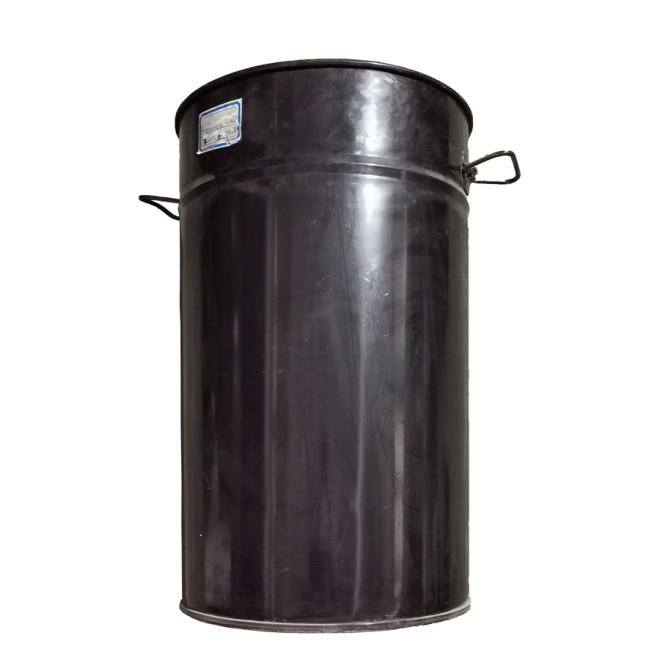
Specialty chemical manufacturing is one of the most demanding industrial sectors when it comes to packaging requirements. Plants handling flammable solvents — including acetone, toluene, methanol, ethanol, xylene, and MEK — must comply with stringent international regulations governing the storage, handling, and transportation of hazardous materials.
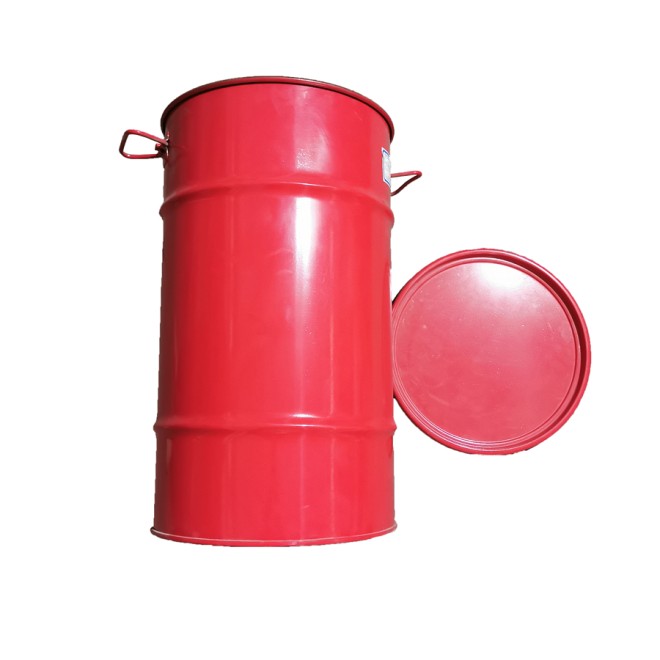
The open head steel drum has emerged as the industry's gold-standard container for these applications. Its fully removable lid provides unmatched access for filling, cleaning, and inspection — a critical advantage when dealing with viscous solvents, reactive intermediates, or materials requiring regular sampling. The robust cold-rolled steel construction offers inherent fire resistance that plastic alternatives simply cannot match.
Global demand for specialty chemicals exceeded USD 620 billion in 2023, with the flammable solvents segment representing a significant and growing portion. As production volumes rise and regulatory frameworks tighten worldwide — particularly under ADR (Europe), DOT 49 CFR (USA), and IMDG (international maritime) standards — the importance of certified, high-performance steel drum packaging has never been greater.
Several converging market forces are accelerating the adoption of open head steel drums across specialty chemical facilities globally. The expansion of pharmaceutical intermediates, agrochemical production, electronic-grade solvents, and specialty coatings industries has created surging demand for reliable, UN-certified packaging that can withstand the rigors of international supply chains.
Simultaneously, environmental and safety regulators in the EU, North America, and Asia-Pacific are imposing stricter requirements on solvent containment. Incidents involving packaging failures — leaks, ruptures, or vapor emissions — carry enormous liability exposure, driving procurement teams to prioritize certified steel drum solutions over cost-cut alternatives.
The Asia-Pacific region, led by China, India, and Southeast Asia, is the fastest-growing market for specialty chemical production. China alone accounts for over 35% of global specialty chemical output, and domestic manufacturers like Foshan Qiaoyue Packaging Co., Ltd. are at the forefront of supplying the certified open head steel drums that this expansion demands.
Open head steel drums serve a diverse range of critical functions across specialty chemical manufacturing — each scenario demanding specific performance characteristics.
Active pharmaceutical ingredient (API) synthesis relies heavily on flammable solvents including isopropanol, ethyl acetate, and dichloromethane. Open head drums allow batch-by-batch sampling and complete product recovery with no residue contamination — critical in GMP-regulated environments. Interior epoxy phenolic linings prevent metal ion leaching that could compromise API purity.
High-performance industrial coatings, UV-curable resins, and automotive refinish products contain solvent blends with flash points below 23°C, classifying them as Class I flammable liquids. Open head steel drums with UN certification and vapor-tight locking ring closures are mandatory for both plant storage and outbound logistics to coatings applicators.
Pesticide, herbicide, and fungicide formulation plants use aromatic solvents (xylene, naphtha) and polar solvents (NMP, DMF) as carriers and co-solvents. These materials are both flammable and environmentally regulated. Steel drums with anti-corrosion internal coatings and leak-proof gasket systems ensure safe containment throughout the formulation-to-distribution chain.
Semiconductor fabs and PCB manufacturers require ultra-pure isopropanol (IPA) and acetone for cleaning processes. The open head design enables cleanroom-compatible dispensing systems to be directly interfaced with the drum. Electropolished internal surfaces and nitrogen-blanketing compatibility make steel drums the preferred choice for electronic-grade solvent packaging.
Printing ink and industrial adhesive production facilities process large volumes of ketone and ester solvents. The wide-mouth open head configuration enables efficient loading of viscous solvent-based formulations and allows thorough drum reconditioning between production campaigns — a significant sustainability and cost advantage in high-volume operations.
Contract chemical manufacturers and solvent distributors require versatile packaging that can handle a rotating portfolio of flammable solvents. Open head steel drums offer the flexibility to be internally coated for specific solvent compatibility, then reconditioned and reused — providing both operational efficiency and reduced environmental footprint compared to single-use alternatives.
Every open head steel drum designed for flammable solvent service incorporates a suite of engineering features that collectively ensure maximum safety and regulatory compliance.
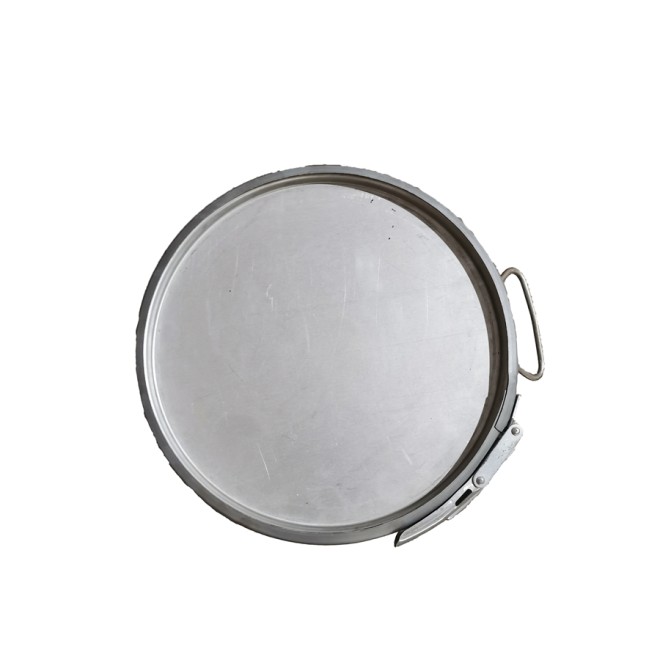
High-torque bolt-ring or lever-lock ring systems create a hermetic seal between the removable head and drum body, preventing vapor escape and maintaining containment integrity under internal pressure fluctuations common with volatile solvents.
All drums carry UN certification (1A2/Y/X) for packing groups II and III flammable liquids, validated through drop, stacking, leakproofness, and hydraulic pressure testing to ensure compliance with ADR, IATA, IMDG, and DOT requirements globally.
Steel drum construction provides inherent electrical conductivity, enabling proper grounding and bonding during solvent transfer operations — a critical safety requirement for preventing electrostatic discharge ignition of flammable vapors.
Premium Q235B cold-rolled carbon steel provides superior dimensional consistency, surface smoothness for effective internal coating adhesion, and excellent mechanical strength — delivering a drum that resists denting, deformation, and structural failure under stacking loads.
Epoxy phenolic, phenolic, or unlined options are available to match specific solvent chemistry. Proper lining selection prevents metal corrosion, maintains product purity, and extends drum service life across multiple use cycles in reconditioning programs.
The open head design enables complete interior access for professional drum reconditioning — including hot-wash cleaning, re-lining, and re-testing — supporting circular economy principles and significantly reducing total cost of ownership for high-volume solvent operations.
In the specialty chemical industry, a packaging failure involving flammable solvents is not merely a product loss event — it is a life safety emergency. The consequences of inadequate drum specification include catastrophic fire and explosion risk, regulatory shutdown of production facilities, criminal liability for responsible officers, and permanent reputational damage.
Procurement teams at specialty chemical plants are increasingly moving away from price-driven drum selection toward total compliance verification. This means demanding full UN certification documentation, third-party test reports, material certificates for steel and coatings, and traceability records from drum manufacturers.
Foshan Qiaoyue Packaging Co., Ltd. provides comprehensive documentation packages with every shipment, giving chemical plant safety managers complete confidence in their packaging compliance posture.
The specialty chemical packaging landscape is evolving rapidly. Understanding these trends helps chemical plants make forward-looking procurement decisions.
Leading specialty chemical companies are implementing closed-loop drum management systems where open head steel drums are collected post-use, professionally reconditioned to UN standards, and returned to service. This reduces packaging waste by up to 80% and cuts per-cycle packaging costs significantly. The open head design is uniquely suited to this model due to its full interior access.
Next-generation steel drums are being equipped with RFID tags and IoT sensors that monitor fill level, temperature, tilt, and location in real time. For flammable solvent applications, this technology enables early leak detection, automated inventory management, and complete chain-of-custody documentation — transforming the humble steel drum into an intelligent asset.
Regulatory bodies worldwide are continuously tightening requirements for flammable liquid packaging. The UN Model Regulations (29th revised edition) introduces updated test protocols, while regional regulations in the EU, China, and India are adding new requirements for vapor pressure testing, compatibility verification, and documentation. Drum manufacturers must invest continuously in testing capabilities to maintain certification currency.
The one-size-fits-all approach to drum specification is giving way to chemistry-specific drum design. Chemical plants are working with drum manufacturers to develop custom internal coating systems optimized for specific solvent families, custom gasket materials for aggressive solvents, and custom closure torque specifications for high-vapor-pressure products.
Post-pandemic supply chain disruptions have accelerated the trend toward regional drum sourcing. Specialty chemical plants are establishing preferred supplier relationships with certified drum manufacturers in their region, reducing lead times from weeks to days and eliminating the risk of supply disruptions that could halt production. Asian manufacturers are particularly well-positioned to serve the rapidly growing Asia-Pacific chemical sector.
ESG reporting requirements are driving specialty chemical companies to evaluate the carbon footprint of their packaging supply chains. Steel drum manufacturers who can demonstrate use of recycled steel content, energy-efficient production processes, and low-VOC coating systems gain a significant competitive advantage as chemical companies seek to reduce Scope 3 emissions.
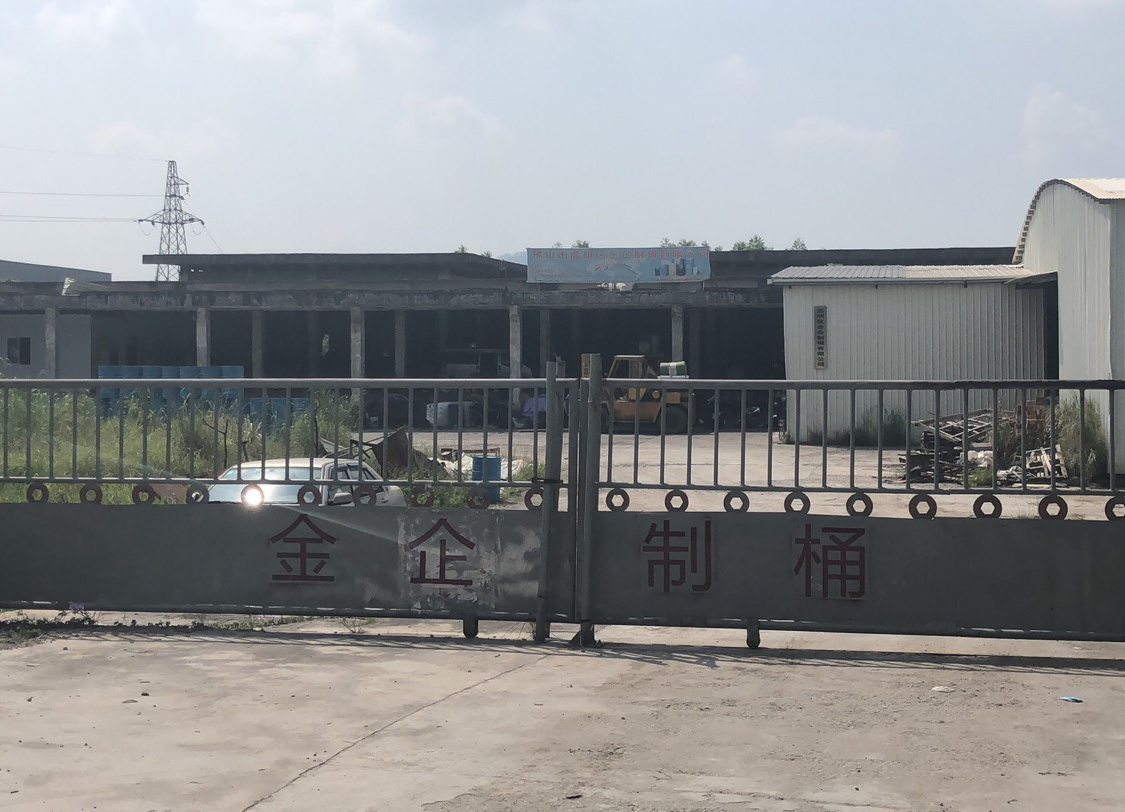
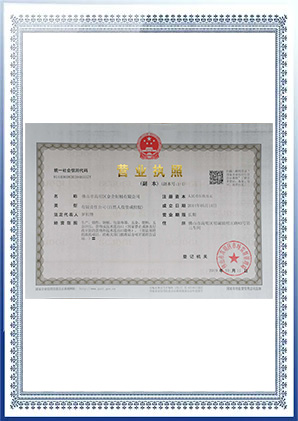
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007 (formerly known as Nanzhuang Ironworks Metal Products Factory). It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning.
We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.
With over 25 years of continuous manufacturing experience and a comprehensive product portfolio spanning 10L to 230L steel drums, we are uniquely positioned to serve specialty chemical plants requiring certified open head steel drums for flammable solvent applications.

We pledge to deliver within agreed deadlines, meet specified standards, and stand by our commitment with our company's reputation as guarantee.

We strive to exceed customer expectations, producing products worthy of their trust.

We offer competitive pricing to serve our broad customer base.

We prioritise client requirements, tailoring our production to meet their specifications.
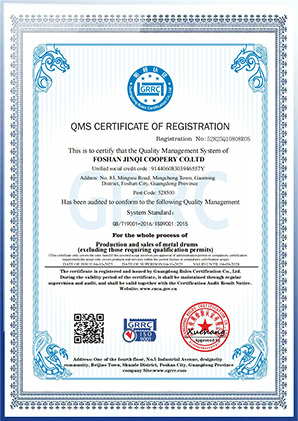
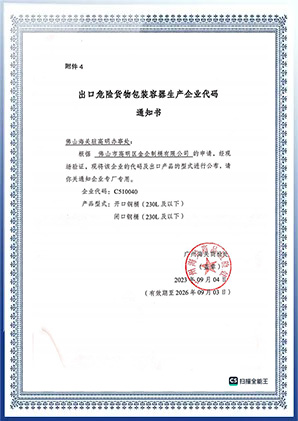
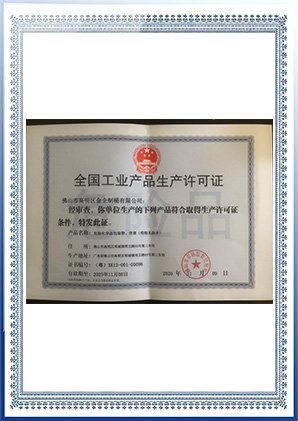
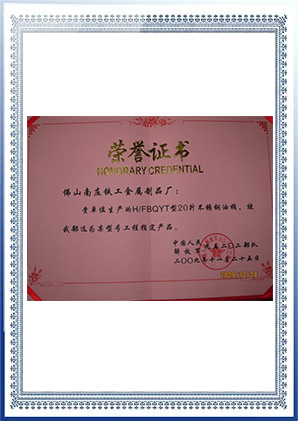
Our steel drums are backed by comprehensive international certifications, validating their suitability for flammable solvent service in specialty chemical plant environments.
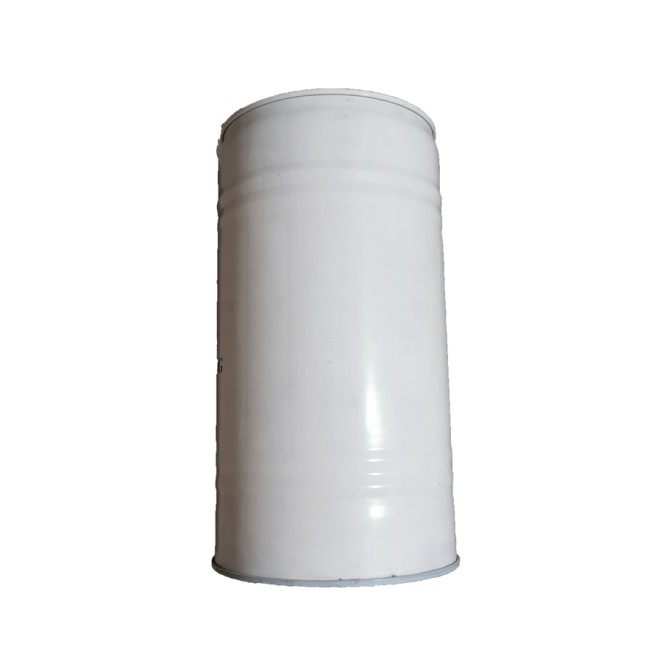
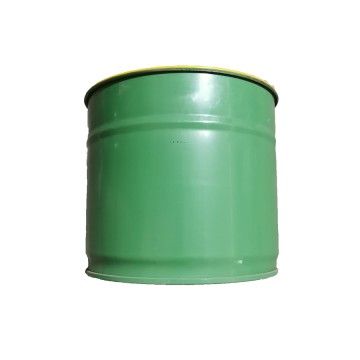
Explore our full portfolio of certified open head and closed head steel drums — engineered for flammable solvent service, hazardous goods transport, and specialty chemical packaging.
Contact Foshan Qiaoyue Packaging Co., Ltd. today to discuss your flammable solvent drum requirements. Our team will provide expert specification guidance, full compliance documentation, and competitive pricing for your volume needs.