Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
Our core product range is purpose-built for bulk food ingredient suppliers and juice concentrate exporters — delivering reliability, compliance, and efficiency at every scale.
The industrial drum market serving food and beverage sectors is experiencing accelerated growth driven by expanding global trade in bulk food ingredients and juice concentrates.
Understanding the commercial and industrial dynamics that make high-quality liquid storage fuel drums essential for bulk food ingredient suppliers and juice concentrate exporters worldwide.
The global trade of bulk food ingredients — including fruit concentrates, vegetable extracts, edible oils, syrups, and flavoring agents — has grown substantially over the past decade. Countries in Asia, South America, and Eastern Europe have emerged as major exporters, requiring millions of reliable storage containers annually. Steel drums remain the preferred choice for long-haul international shipments due to their structural integrity, chemical resistance, and ability to maintain product purity across extended transit periods.
The global juice concentrate market is projected to exceed $90 billion by 2028, driven by demand from beverage manufacturers, food processors, and health supplement producers. Exporters of apple, orange, grape, mango, and berry concentrates require FDA-compliant, food-grade steel drums that prevent oxidation, contamination, and flavor degradation. Sealed, epoxy-lined, or stainless steel drums are increasingly specified in export contracts to meet stringent international food safety standards including HACCP, BRC, and ISO 22000.
Modern liquid storage drums are engineered to serve dual-purpose roles — handling both food-grade liquids and industrial fluids such as lubricants, fuel additives, and chemical concentrates. This versatility has made multi-specification drum manufacturing a strategic advantage. Manufacturers who can produce both UN-certified industrial drums and food-grade containers under one roof — like Foshan Qiaoyue Packaging — offer significant supply chain efficiencies to exporters managing diverse product portfolios.
From farm-to-factory to port-to-processor, our drums are engineered for the most demanding liquid containment challenges across the global food and industrial supply chain.
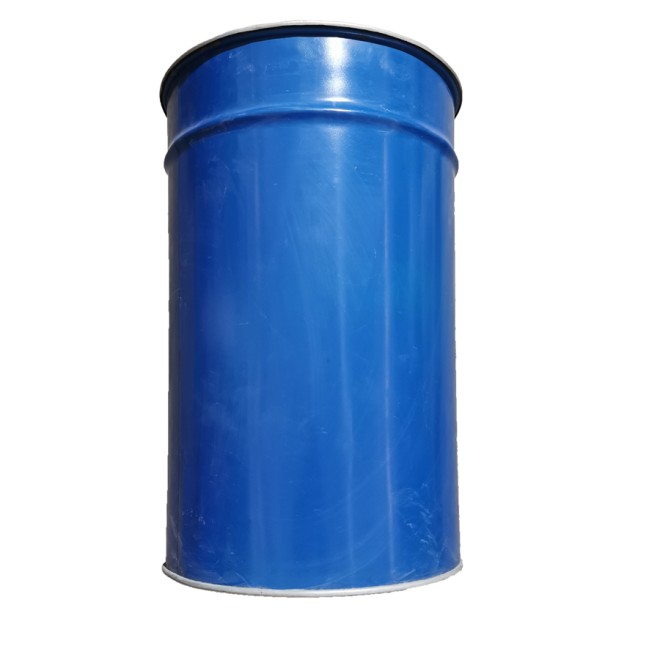
High-Brix juice concentrates require airtight, corrosion-resistant containers during refrigerated shipping. Our closed-top steel drums with epoxy or food-grade lacquer linings prevent oxidation and maintain flavor profiles across 30–60 day ocean freight journeys. The 60L Blue Conical Epoxy-Lined Metal Drum is particularly suited for this application, offering leak-proof sealing and stackable geometry for container optimization.
Palm oil, sunflower oil, and coconut oil suppliers require drums that can withstand high-temperature filling (up to 80°C) and maintain structural integrity during solidification cycles. Our galvanized and stainless steel drums offer superior thermal resistance and are compatible with automated filling lines used by major edible oil processors in Southeast Asia and West Africa.
Flavor houses and food additive manufacturers require small-to-medium capacity drums (10L–30L) for precise batch storage of high-value concentrates, natural extracts, and enzymatic solutions. Our 30L White Necked Closed Steel Drum and 10L Stainless Steel variants provide the contamination-free environment required for these sensitive materials, with smooth interior surfaces that allow complete product evacuation and easy cleaning.
Packaging manufacturers and construction material suppliers utilize specialized open-top drums for hot-melt adhesives, waxes, and thermoplastic compounds. The 20L Collapsible-Bottom Open-Top Hot Melt Adhesive Drum with Handles is engineered specifically for this use case — the collapsible bottom design allows complete product extraction without waste, while the dual-handle configuration ensures safe handling of heated contents.
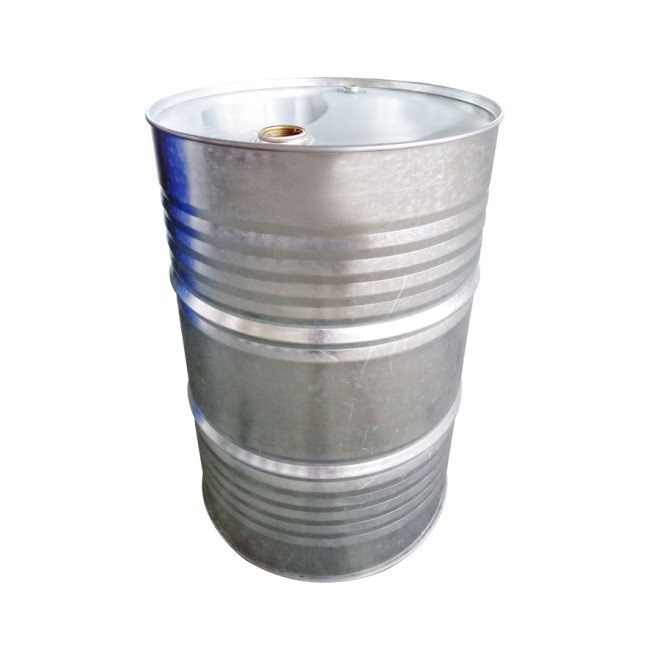
Petroleum distributors, mining operations, and agricultural machinery suppliers require robust 200L+ drums for diesel, lubricating oils, and hydraulic fluids. Our 200–230L Galvanised Closed-Top Steel Drum meets UN certification requirements for hazardous liquid transport, offering crimped seams, bung-sealed openings, and anti-corrosion galvanized coatings that extend service life in harsh outdoor storage environments.
Chemical exporters face complex regulatory requirements across different markets. Our drums are manufactured to comply with IMDG (International Maritime Dangerous Goods) codes, ADR regulations for European road transport, and OSHA standards for workplace storage. The corrugated iron drum series provides additional structural reinforcement for high-density liquid chemicals, while the stainless steel conical drum series serves pharmaceutical-grade chemical applications requiring zero contamination tolerance.
The industrial drum sector is undergoing significant transformation as sustainability mandates, digital supply chains, and evolving food safety regulations reshape buyer expectations globally.
Major food multinationals are mandating drum reconditioning programs to reduce packaging waste. Reconditioned steel drums — cleaned, re-coated, and re-certified — now represent a growing segment of the market. Manufacturers offering durable, reconditionable drum designs gain competitive advantage as sustainability becomes a procurement criterion alongside price and lead time.
Forward-thinking exporters are integrating RFID tags and QR code systems into drum packaging for end-to-end traceability. This enables real-time tracking of liquid inventory across global supply chains, reduces loss from misplaced containers, and supports blockchain-based food provenance verification increasingly required by premium retail buyers in Europe and North America.
New-generation epoxy phenolic, BPA-free, and water-based lacquer coatings are replacing traditional interior linings to meet evolving food contact material regulations. These coatings extend drum service life, prevent flavor migration in juice concentrates, and comply with EU Regulation 10/2011 and FDA 21 CFR requirements — increasingly becoming standard specifications in export contracts.
Leading drum manufacturers are investing in CNC-controlled roll-forming, robotic welding, and automated seam-sealing systems to achieve tighter dimensional tolerances and consistent quality across high-volume production runs. This automation reduces defect rates below 0.1% — critical for food exporters who cannot afford product loss from container failures during ocean freight.
The rise of direct-to-consumer food ingredient platforms is driving demand for smaller-format drums (10L–30L) with enhanced branding capabilities. Custom color coding, embossed logos, and tamper-evident closure systems are becoming standard requirements as food ingredient suppliers differentiate their products in increasingly competitive online marketplaces across Southeast Asia, the Middle East, and Africa.
Asia-Pacific remains the fastest-growing region for industrial drum consumption, driven by expanding food processing capacity in China, India, Vietnam, and Indonesia. The region's juice concentrate export sector — particularly for tropical fruits — is generating substantial demand for food-grade steel drums that meet both domestic standards and the import requirements of destination markets in the EU, USA, and Middle East.
Foshan's leading manufacturer of diversified industrial and food-grade drum solutions — serving global clients with quality, integrity, and innovation since 1999.
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007 (formerly known as Nanzhuang Ironworks Metal Products Factory). It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning.
We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.
As Foshan's only full-spectrum drum manufacturer, we bridge the gap between industrial-grade durability and food-grade compliance — making us the preferred partner for bulk food ingredient suppliers and juice concentrate exporters who demand uncompromising container performance on the global stage.
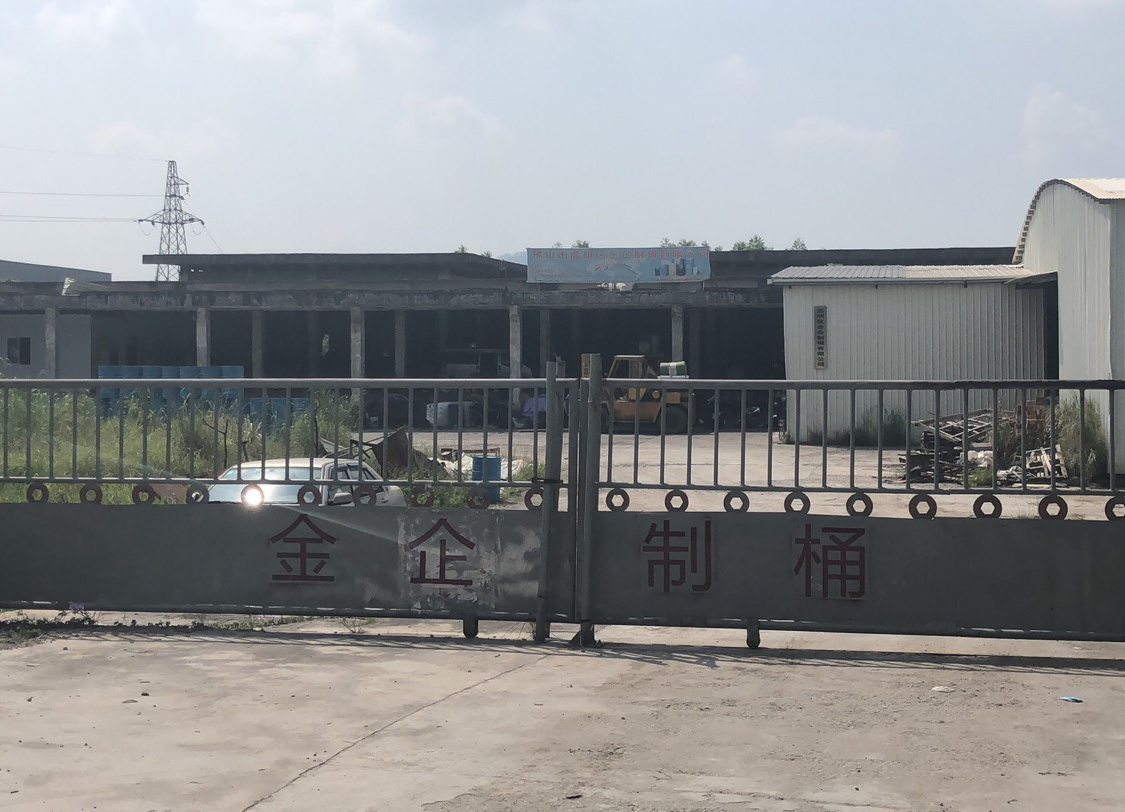

We pledge to deliver within agreed deadlines, meet specified standards, and stand by our commitment with our company's reputation as guarantee.

We strive to exceed customer expectations, producing products worthy of their trust.

We offer competitive pricing to serve our broad customer base.

We prioritise client requirements, tailoring our production to meet their specifications.
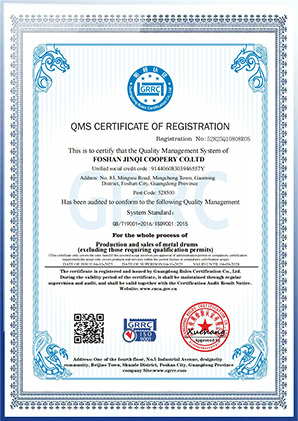
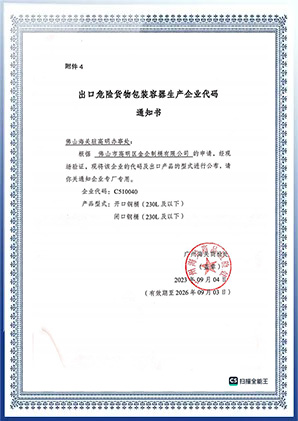
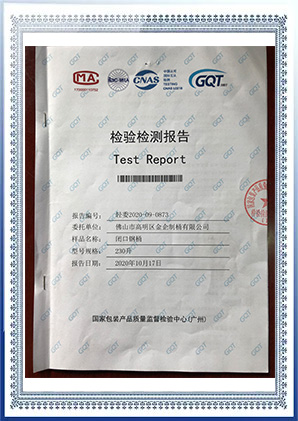
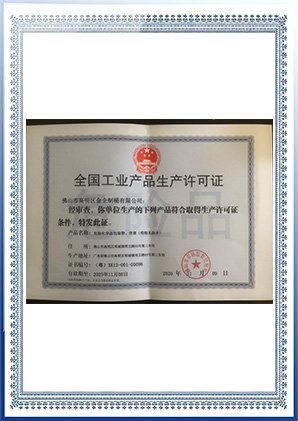
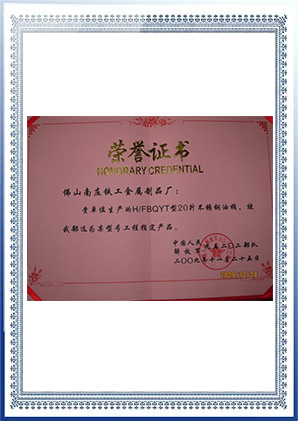
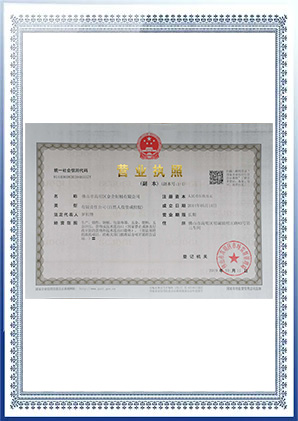
Our quality management systems and product certifications reflect our commitment to international compliance standards for food-grade and industrial liquid storage solutions.
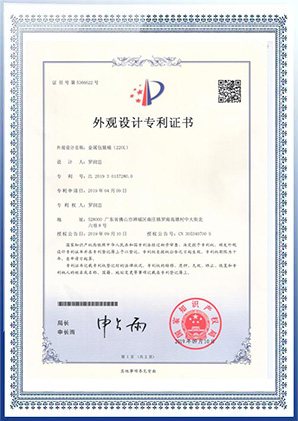
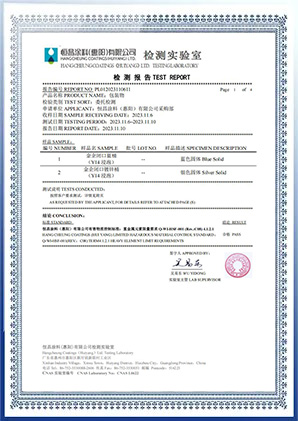
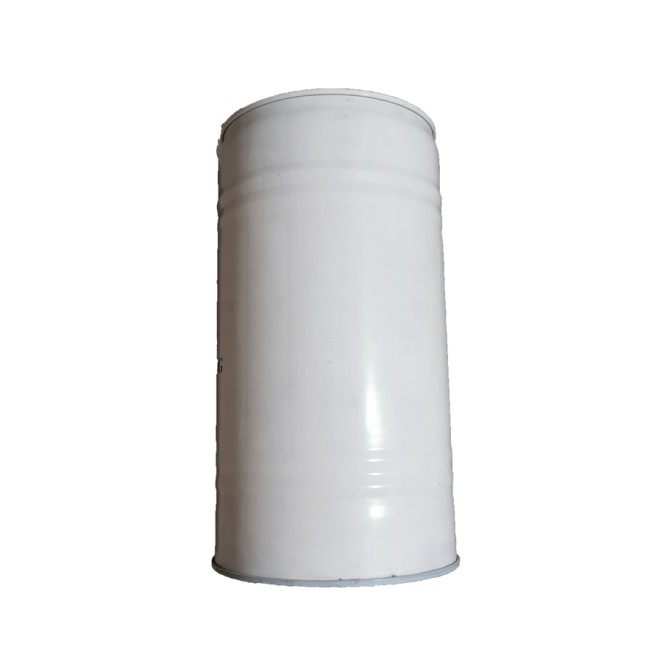
Explore our full product portfolio — from compact 10L stainless steel drums for precision food ingredient storage to heavy-duty 200L galvanized drums for bulk fuel and chemical export.
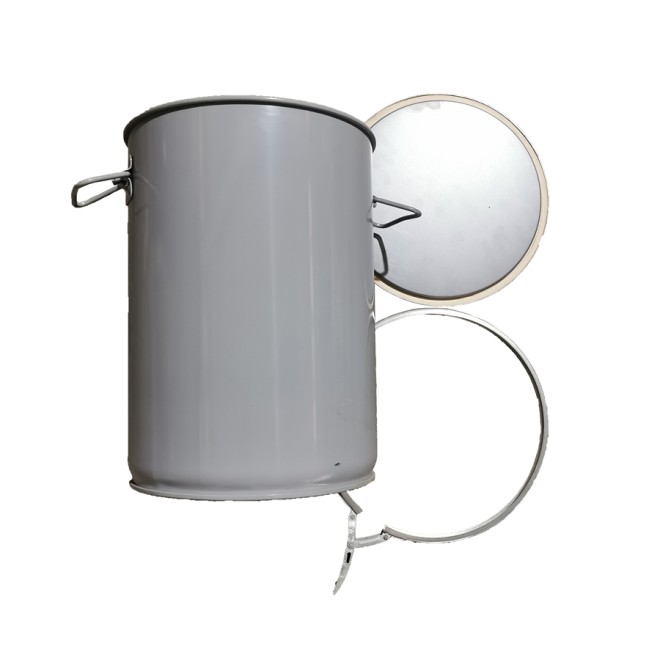
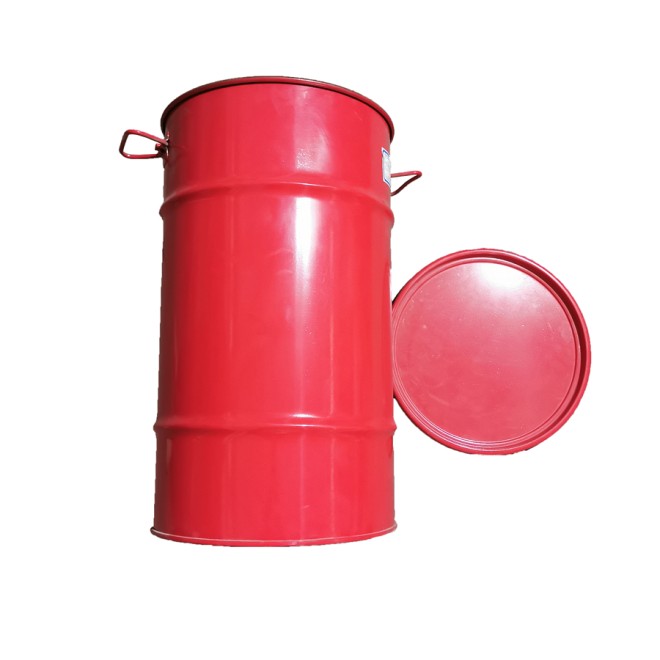
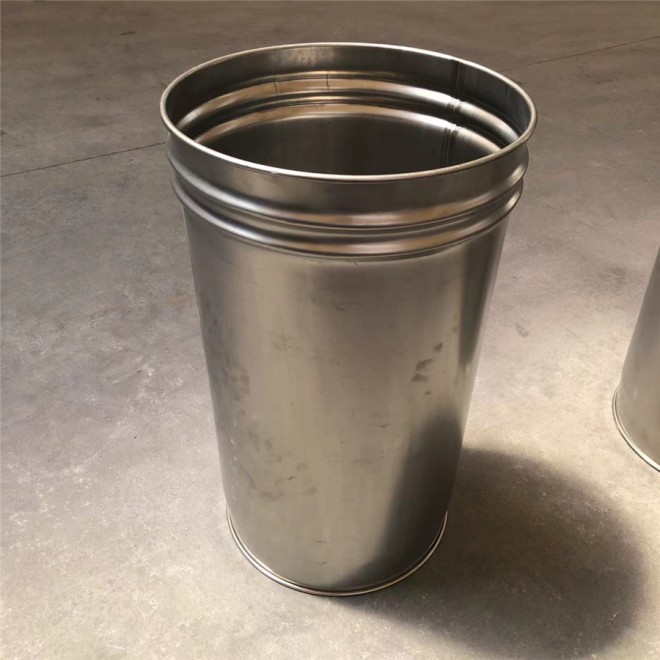
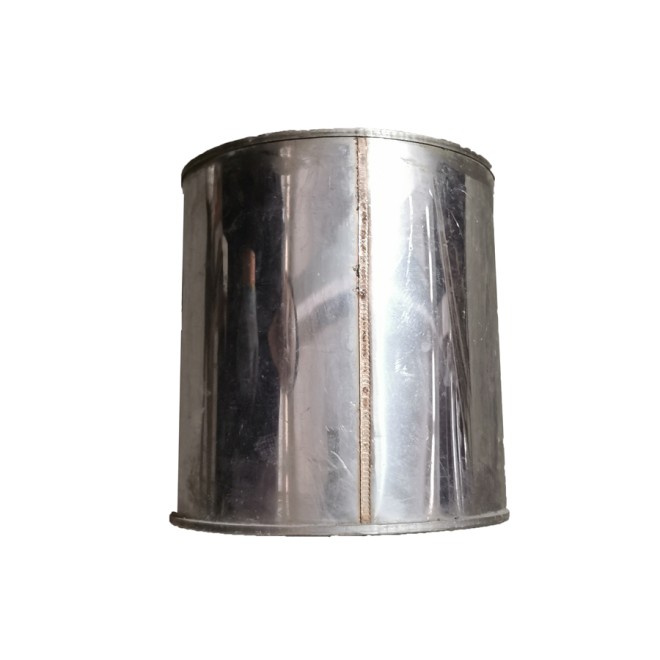
Partner with Foshan Qiaoyue Packaging — Foshan's only full-spectrum drum manufacturer — for food-grade, industrial, and fuel storage solutions that meet global compliance standards. Custom specifications, competitive pricing, and reliable delivery guaranteed.
Request a Quote Today →