Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
Select, high-performance drum configurations designed to meet rigorous pharmaceutical standards for sterile liquid ingredients.
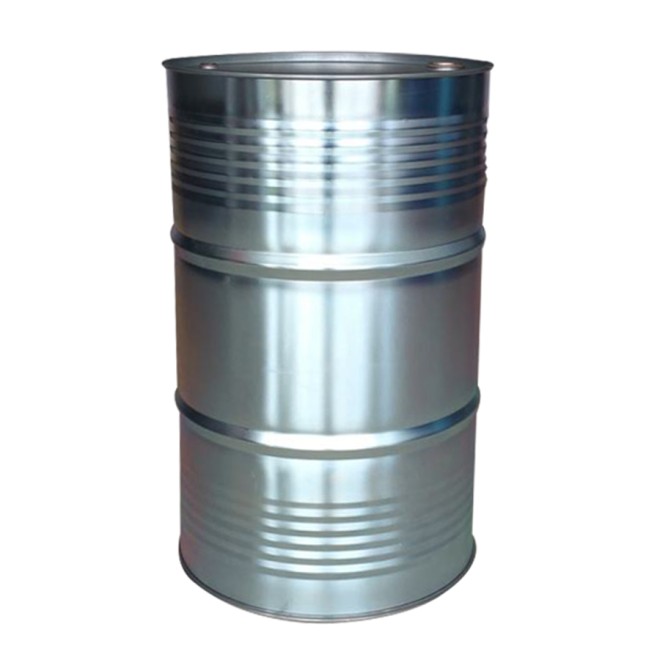
In the modern pharmaceutical industry, maintaining the absolute purity of sterile liquid ingredients is paramount. Active Pharmaceutical Ingredients (APIs), biological buffers, sterile intermediates, and vaccine bases represent millions of dollars in research and manufacturing value. The containment systems used to transport and store these fluids must offer more than simple structural integrity; they must function as active barriers against microbial contamination, chemical interaction, and environmental degradation. The industrial chemical drum, specifically optimized for sterile liquid ingredients, stands as a cornerstone of this high-stakes logistics chain.
Zero-tolerance barrier protection preventing microbial ingress, particulate contamination, and cross-batch degradation.
Electropolished stainless steel and high-grade coatings ensure zero leaching or reaction with active ingredients.
Manufactured in alignment with cGMP, FDA regulations, and international UN ratings for hazardous/sterile fluid transport.
The global pharmaceutical packaging market is undergoing a rapid evolution. With the rise of biopharmaceuticals, personalized medicine, and advanced mRNA-based therapies, the demand for high-purity fluid handling solutions has surged. Traditionally, glass carboys and plastic containers dominated minor fluid containment. However, these materials present significant risks: glass is fragile and susceptible to thermal shock, while plastics present risks of extractables and leachables (E&L) that can alter the chemical composition of sensitive liquid ingredients.
Consequently, high-performance industrial chemical drums—particularly those fabricated from stainless steel (grades 304, 316L) and specialized cold-rolled steel—have become the industry standard. These drums offer the mechanical strength to withstand high-pressure sterilization cycles (such as autoclaving or Clean-in-Place/Sterilize-in-Place systems) while maintaining dimensional stability. Commercially, pharmaceutical manufacturers are prioritizing suppliers that can guarantee traceability, surface roughness optimization (Ra values below 0.4 µm), and robust testing certifications.
Industrial chemical drums configured for sterile liquid ingredients find application in several critical phases of the pharmaceutical lifecycle:
Looking to the future, three major trends are shaping the industrial chemical drum sector for pharmaceutical applications:
1. The Shift Toward Reusable Stainless Steel: While single-use plastic bags have gained popularity, their environmental footprint and the risk of microplastic contamination are driving companies back to reusable, high-grade stainless steel drums. These drums offer a lifespan of decades, can be continuously sterilized, and are 100% recyclable, aligning with global corporate sustainability goals.
2. Integration of Smart Tracking (IoT): Modern logistics demand real-time data. Advanced industrial drums are now being designed with integrated RFID chips and IoT sensors that monitor temperature, pressure, and location. This ensures that sterile liquid ingredients remain within predefined thresholds throughout the entire cold chain.
3. Advanced Surface Treatments: To prevent adhesion of expensive biological fluids to the drum walls, manufacturers are applying advanced electropolishing and hydrophobic inner coatings. This maximizes product recovery during dispensing and simplifies the cleaning process, reducing chemical and water usage in cleaning cycles.
Foshan Qiaoyue Packaging Co., Ltd. (formerly known as Nanzhuang Ironworks Metal Products Factory)
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007. It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning. We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.
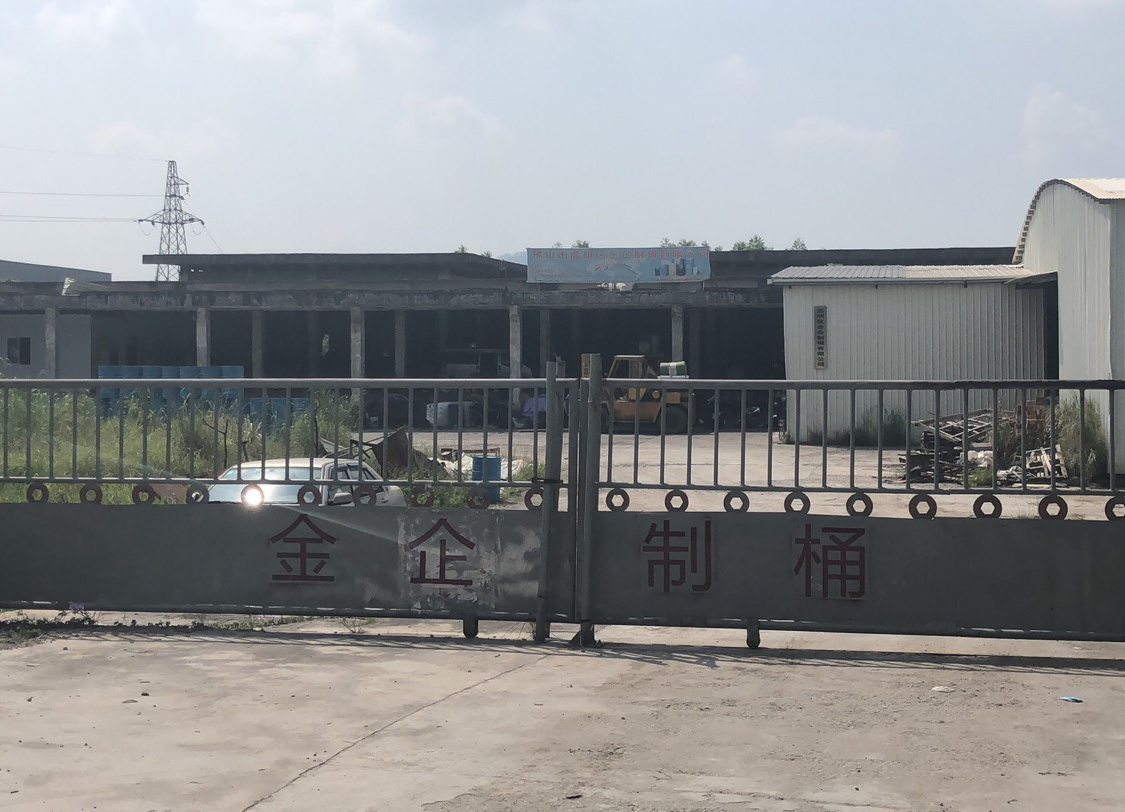

We pledge to deliver within agreed deadlines, meet specified standards, and stand by our commitment with our company's reputation as guarantee.

We strive to exceed customer expectations, producing products worthy of their trust.

We offer competitive pricing to serve our broad customer base.

We prioritise client requirements, tailoring our production to meet their specifications.
Our commitment to quality is backed by international manufacturing and material standards.
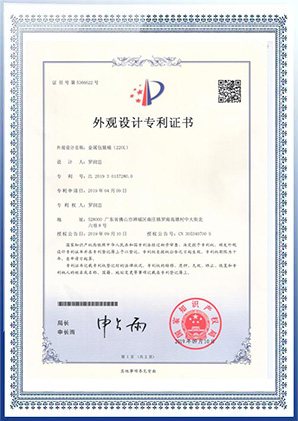
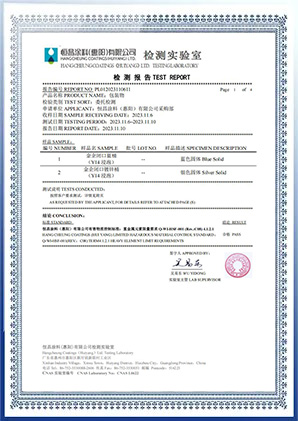
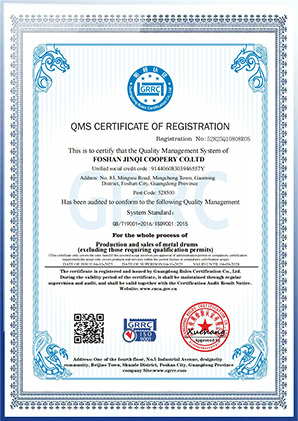
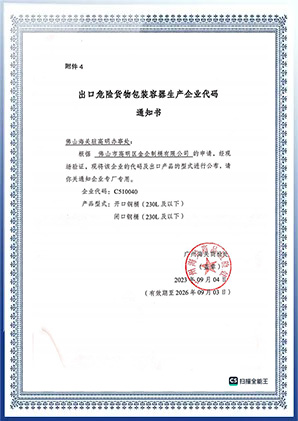
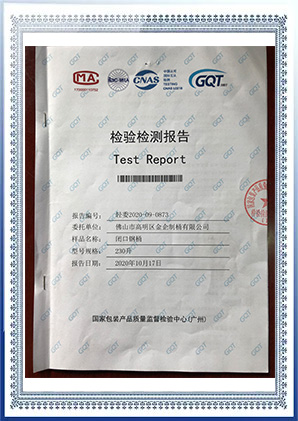
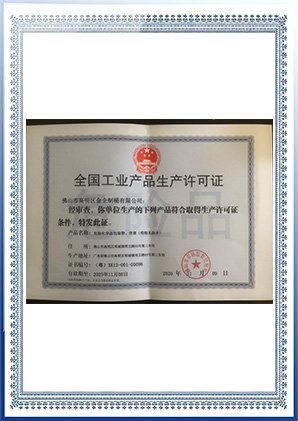
Explore our full range of customizable containment products designed for various liquid and solid ingredient storage requirements.