Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
Explore our top-tier industrial drum solutions engineered for food-grade chemical and juice concentrate applications.
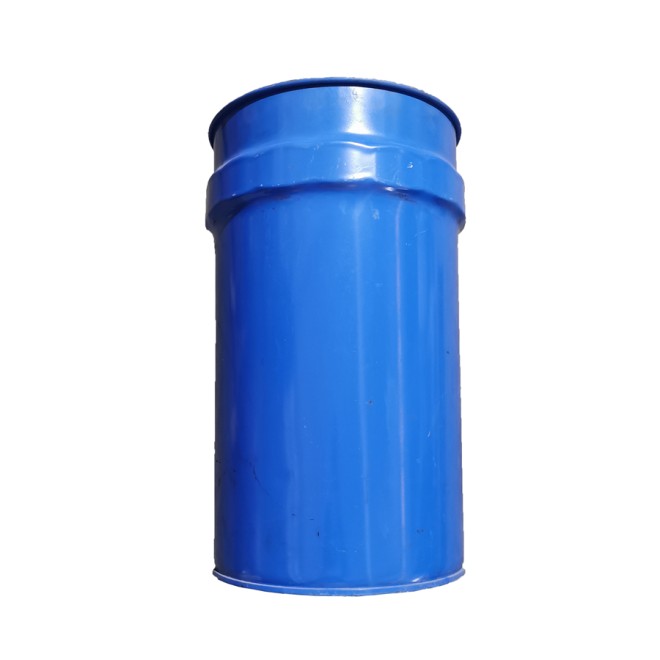 Bulk Powder / Food Ingredient
70L Large Conical Drum — Bulk Food Powder & Ingredient Packaging Drum
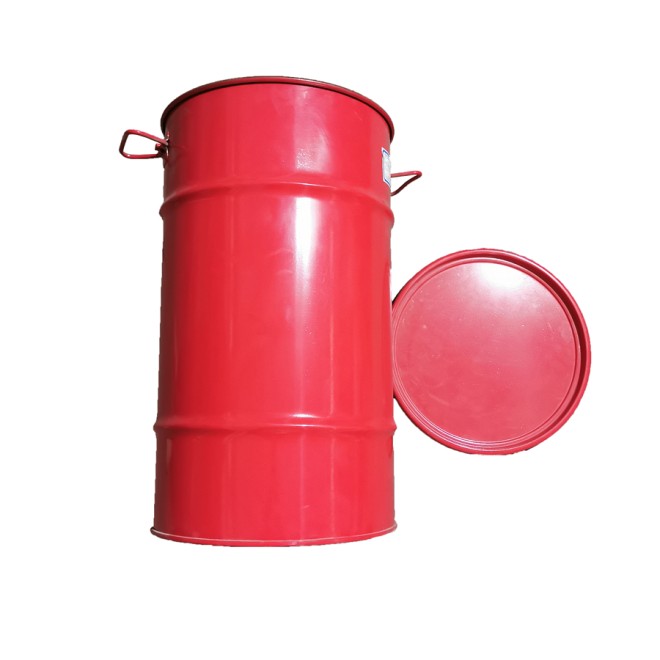 Juice Concentrate Export
50L Red Open-Top Corrugated Iron Drum — Juice Concentrate Export Packaging
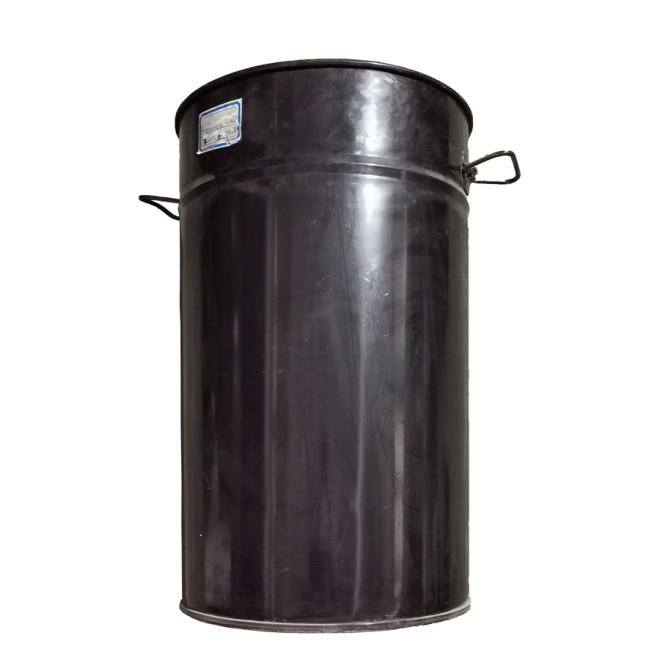 Chemical Food Storage
60L Black Sealed Open-Top Drum — Q235B Steel for Food Chemical Ingredient Storage
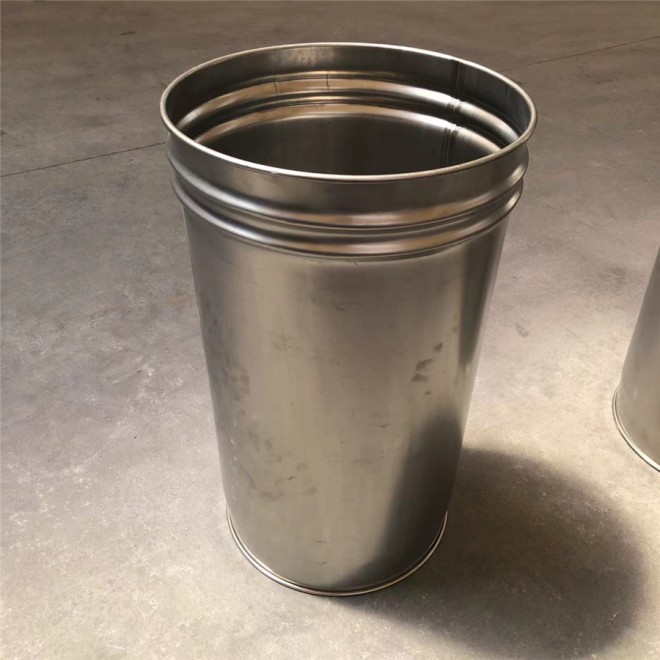 Food-Grade Stainless
Stainless Steel Conical Drum — Premium Food-Grade & Juice Concentrate Solution
The global bulk food ingredient and juice concentrate industry has experienced remarkable growth over the past decade, driven by expanding consumer markets across Asia-Pacific, the Middle East, and Latin America. As international trade volumes surge, the demand for reliable, food-safe, and export-compliant industrial chemical drums has never been greater.
Industrial chemical drums — including steel, stainless steel, and corrugated iron variants — serve as the backbone of liquid and powder food ingredient logistics. From concentrated fruit juices and flavour extracts to food-grade acidulants and preservatives, these drums ensure product integrity across long-haul shipping routes, temperature fluctuations, and rigorous customs inspections.
According to industry analysts, the global industrial packaging market for food and beverage applications is projected to exceed USD 78 billion by 2030, with steel and stainless drums accounting for a significant share due to their superior barrier properties, recyclability, and compliance with international food safety standards such as FDA 21 CFR and EU Regulation 10/2011.
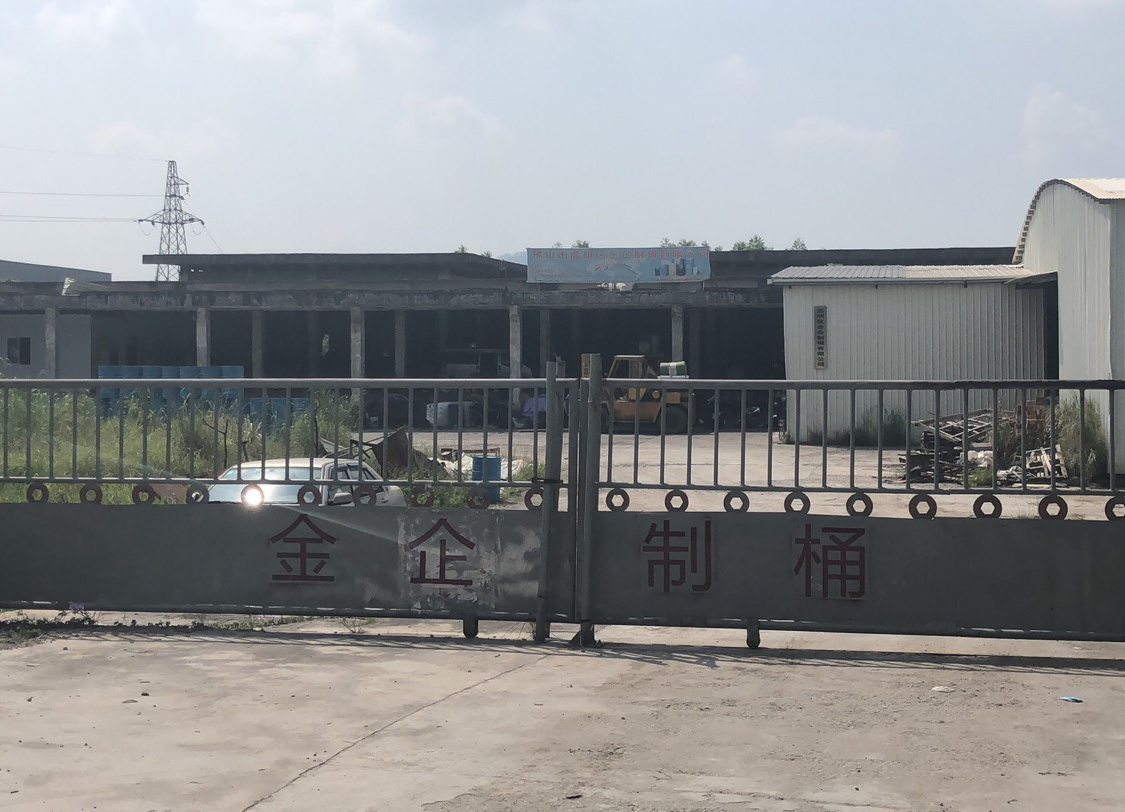
Purpose-engineered packaging that meets the strictest food safety, chemical compatibility, and export logistics requirements.
Meets FDA, EU, and GB standards for direct and indirect food contact — essential for juice concentrate and bulk ingredient exporters.
Cold-rolled Q235B carbon steel and 304/316 stainless steel construction withstands stacking, vibration, and pressure during ocean freight.
Steel drums offer the highest recyclability rate of any packaging material — a key factor for ESG-conscious food exporters and buyers.
UN-certified drum options available for hazardous food chemicals, meeting IMDG, ADR, and IATA transport regulations worldwide.
The intersection of food safety regulation, supply chain digitalisation, and sustainability is redefining how industrial drums are designed, manufactured, and deployed.
Leading food exporters are adopting IoT-enabled drum tracking solutions — embedding RFID tags and QR codes on steel drums to monitor temperature, location, and tamper status in real time throughout the cold chain. This technology is rapidly becoming a baseline requirement for premium juice concentrate buyers in the EU and North America.
Regulatory pressure from the EU Green Deal and China's dual-carbon policy is accelerating the shift toward reusable and fully recyclable steel drums. Bulk food ingredient suppliers are increasingly specifying stainless steel conical drums for multi-trip logistics, reducing single-use plastic and lowering carbon footprint across the supply chain.
New-generation epoxy phenolic and polyurethane internal linings are enabling steel drums to safely contain highly acidic juice concentrates (pH < 3) and reactive food-grade chemicals without contamination risk. This expands the application scope of conventional steel drums into previously stainless-steel-only segments.
CNC roll-forming, robotic welding, and automated leak-testing lines are raising quality consistency while reducing lead times. Manufacturers investing in Industry 4.0 production lines can now offer tighter dimensional tolerances and faster custom order fulfilment — a competitive advantage for global food ingredient exporters requiring just-in-time packaging.
The market is shifting away from one-size-fits-all 200L drums toward a broader spectrum of capacities — from 10L sealed steel drums for specialty flavour extracts to 230L stainless conical drums for large-volume juice concentrate shipments. Customisation in closure type, handle design, and surface treatment is now standard expectation.
Major food ingredient and juice concentrate exporters are consolidating their drum procurement to fewer, more capable suppliers to ensure consistency in quality, certification, and supply continuity. This trend favours established manufacturers with diversified product ranges, multi-standard certifications, and proven export track records.
From tropical juice processing plants to multinational food additive distributors, our drums serve the most demanding real-world packaging challenges.
Orange, apple, mango, and tropical fruit juice concentrate exporters require drums that maintain seal integrity at temperatures ranging from -18°C (frozen concentrate) to +20°C (ambient NFC). Our stainless steel conical drums and sealed steel drums with food-grade linings are purpose-built for both cold-fill and aseptic filling lines, ensuring zero flavour migration and full compliance with Codex Alimentarius standards.
Suppliers of bulk food ingredients such as maltodextrin, citric acid, sodium bicarbonate, food-grade phosphates, and flavour powders rely on our 70L large conical drums and sealed steel drums to prevent moisture ingress, caking, and contamination during warehouse storage and international shipping. The conical drum geometry facilitates complete product discharge, minimising residue waste.
Food-grade chemicals including acetic acid, lactic acid, sodium benzoate solutions, and potassium sorbate require packaging that combines chemical resistance with food safety compliance. Our Q235B cold-rolled steel drums with epoxy lining and our 304-grade stainless steel open-top drums provide the ideal combination of barrier performance, regulatory compliance, and cost efficiency for chemical food additive exporters.
For bulk food ingredient suppliers shipping FCL or LCL containers across transoceanic routes, drum stacking strength, UN certification, and corrosion resistance are non-negotiable. Our corrugated iron drums with dual handles and cold-rolled steel band construction are engineered for high stack-load scenarios, while stainless steel conical drums offer the premium solution for high-value concentrate shipments requiring maximum product protection.
Within large-scale food processing facilities, industrial drums serve as critical intermediate bulk containers (IBCs) for raw ingredient intake, in-process storage, and finished product holding. The ergonomic dual-handle designs on our 50L and 60L drums facilitate safe manual handling, while the open-top configurations allow efficient filling and cleaning-in-place (CIP) operations compliant with HACCP protocols.
Rapidly growing food import markets in Southeast Asia, the Gulf Cooperation Council, and Sub-Saharan Africa are driving demand for cost-effective yet reliable drum packaging. Our 30L white necked closed steel drums and 10L green necked sealed steel drums with handles are ideally sized for the smaller-batch distribution networks characteristic of these markets, offering brand-customisable surface printing and multi-language labelling compatibility.
For bulk food ingredient suppliers and juice concentrate exporters, the drum is not merely a container — it is a quality statement, a compliance instrument, and a logistics asset. Selecting a drum manufacturer with proven multi-standard certification, diversified product capability, and a commitment to continuous innovation directly impacts product quality, regulatory approval timelines, and total landed cost. Foshan Qiaoyue Packaging Co., Ltd. has been that trusted partner for global food exporters since 1999.
25+ years of manufacturing excellence, serving bulk food ingredient suppliers and juice concentrate exporters across 120+ countries.
As Foshan's sole manufacturer capable of producing diverse types of drum products, we offer the broadest portfolio — from 10L specialty drums to 230L stainless conical drums — under one roof, simplifying procurement for complex export packaging programmes.
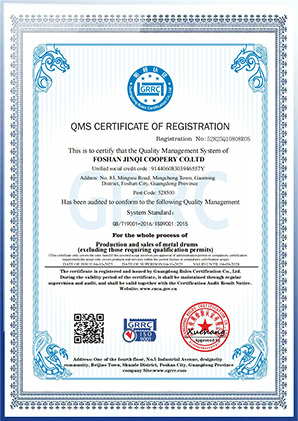
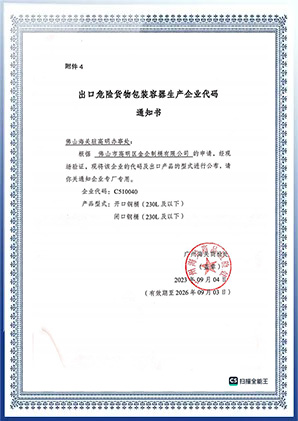
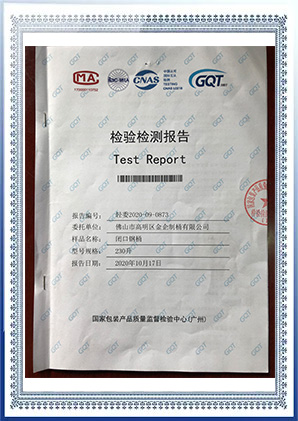
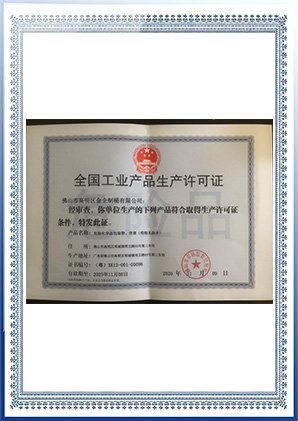
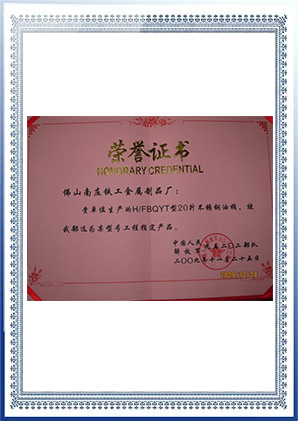
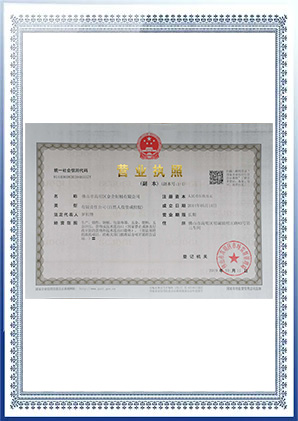
Our drums are certified across international quality, safety, and food-contact standards, enabling seamless import clearance in the EU, USA, Middle East, and ASEAN markets. Certificate documentation is provided with every shipment.
From custom capacities and closure configurations to branded surface printing and special coatings, our 50+ person specialist team delivers tailored drum solutions with competitive lead times — aligned to your production schedule and export calendar.
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007 (formerly known as Nanzhuang Ironworks Metal Products Factory). It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning. We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.
The values that drive every drum we manufacture and every customer relationship we build.

We pledge to deliver within agreed deadlines, meet specified standards, and stand by our commitment with our company's reputation as guarantee.

We strive to exceed customer expectations, producing products worthy of their trust.

We offer competitive pricing to serve our broad customer base.

We prioritise client requirements, tailoring our production to meet their specifications.
Our comprehensive certification portfolio demonstrates unwavering commitment to international quality and food safety standards.
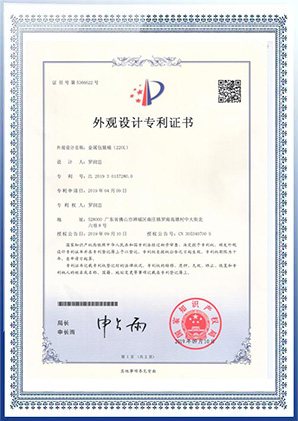
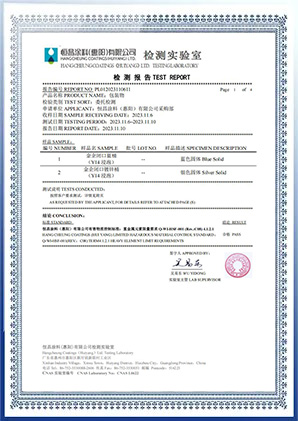
From compact specialty drums to large-volume stainless conical solutions — the full portfolio for every export packaging requirement.
Bulk Ingredient Drum
70L Large Conical Drum Packaging Drum Specifically for Powder Coating Paint
Juice Concentrate Export
50L Red Open-Top Corrugated Iron Drum with Dual Handles
Food Chemical Storage
60L Black Sealed Open-Top Drum with Q235b Cold-Rolled Carbon Steel Band and Handles
Food-Grade Stainless
Stainless Steel Conical Drum
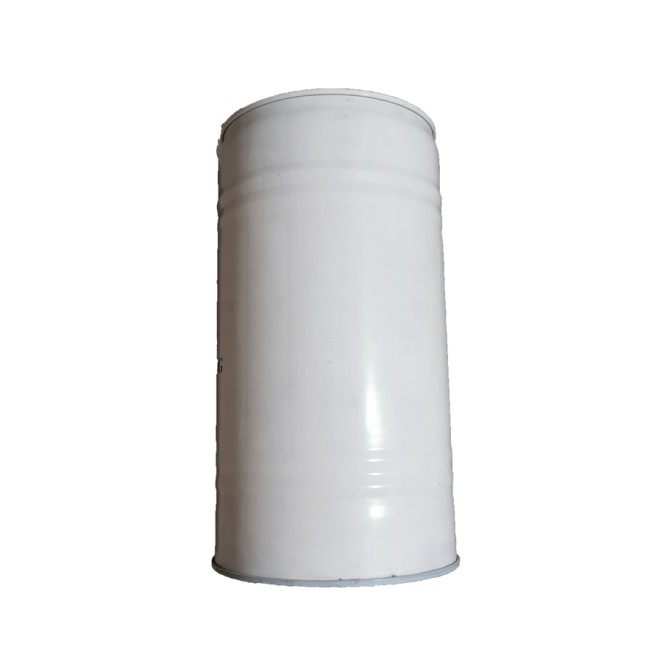 Specialty Ingredient Drum
30L White Necked Closed Steel Drum with Handle
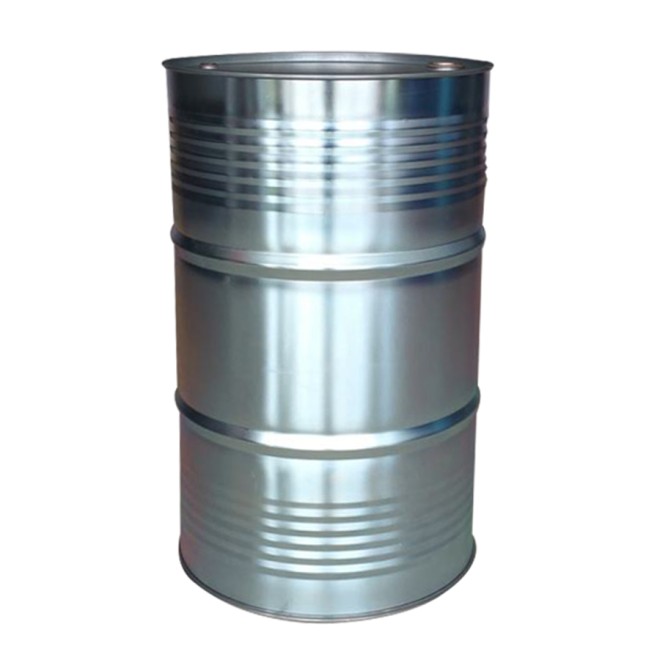 Large Volume Concentrate
200-230L Stainless Steel Conical Closed-Top Drum
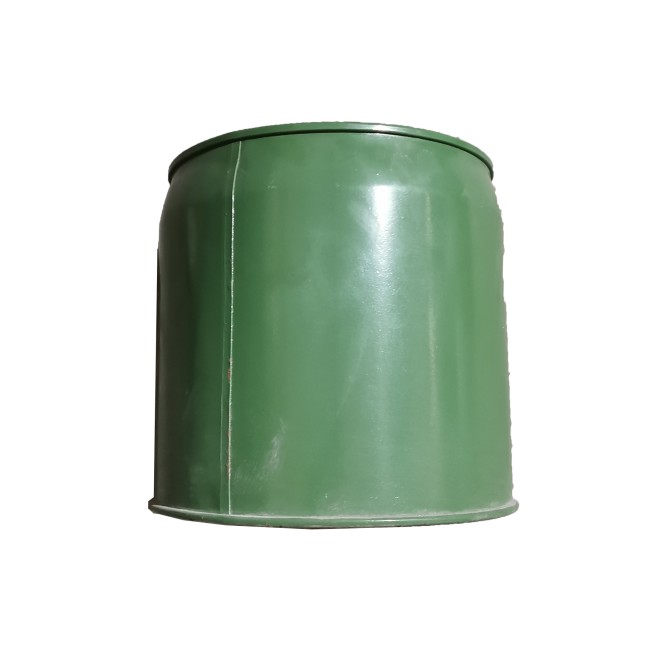 Flavour Extract Packaging
10L Green Necked Sealed Steel Drum with Handle
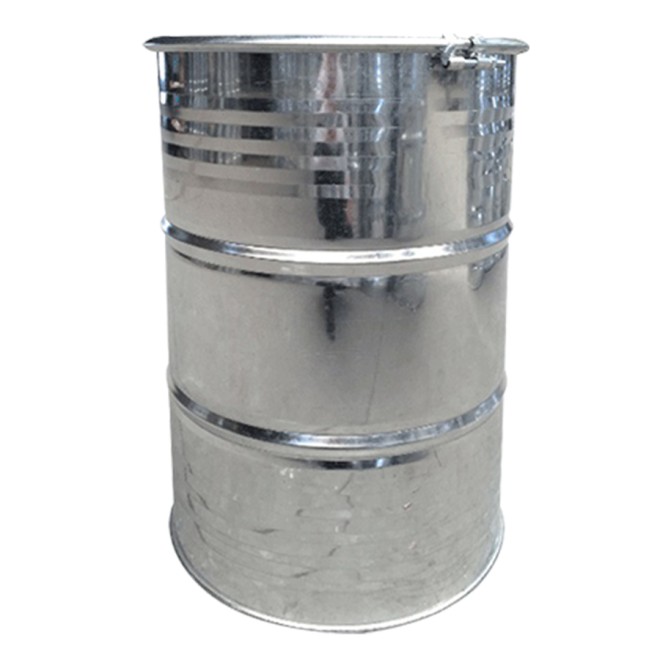 Bulk Juice Export
200–230L Stainless Steel Open-Top Drum
Partner with Foshan Qiaoyue Packaging — your trusted industrial chemical drum manufacturer for export-ready, food-safe, and certified packaging solutions since 1999.
Contact Us Today