Leave Your Message
-
 Get Your Quote
-
 Email
-
Phone
Explore our most popular drum solutions engineered specifically for industrial paint and architectural coating applications.
The global industrial paint and architectural coating market has experienced robust and sustained growth over the past decade, driven by rapid urbanisation, expanding infrastructure investment, and rising demand for high-performance protective and decorative surface solutions. According to leading industry analysts, the architectural coatings segment alone is projected to exceed USD 100 billion in value by 2028, while industrial coatings — encompassing automotive, marine, aerospace, and heavy machinery applications — continue to outpace broader manufacturing sector growth rates.
Paint and coating manufacturers face a fundamental challenge: their products are chemically active, often volatile, and highly sensitive to contamination, moisture, and oxygen exposure. The integrity of the packaging drum is not merely a logistical concern — it is a direct determinant of product quality, shelf life, and end-user safety. Galvanized chemical drums have emerged as the preferred packaging standard precisely because they address all of these challenges simultaneously.
Galvanized steel drums — coated with a protective zinc layer through hot-dip or electrolytic galvanisation processes — offer a compelling combination of mechanical robustness, chemical resistance, and cost-effectiveness that alternative materials such as HDPE plastic or plain steel simply cannot match in demanding industrial environments. For manufacturers of architectural coatings, industrial paints, powder coatings, and specialty chemical formulations, selecting the right drum is a strategic decision that affects supply chain efficiency, product integrity, regulatory compliance, and brand reputation.
Several macro-level forces are converging to accelerate demand for high-quality galvanized chemical drums within the paint and coatings manufacturing sector. First, the global construction boom — particularly across Southeast Asia, the Middle East, and Sub-Saharan Africa — is generating unprecedented volumes of architectural coating production, requiring scalable and reliable bulk packaging. Second, increasingly stringent environmental and transport regulations (including UN certification requirements for hazardous goods packaging) are compelling manufacturers to upgrade from commodity-grade containers to certified, traceable drum solutions. Third, the rise of e-commerce distribution channels for professional-grade coatings is creating new requirements for drums that withstand extended transit conditions and multiple handling cycles without compromising seal integrity.
Additionally, the shift toward water-based and low-VOC (volatile organic compound) coating formulations — driven by tightening environmental legislation in the EU, North America, and China — is reshaping drum specification requirements. Water-based coatings are particularly susceptible to bacterial contamination and freeze-thaw damage, making the superior thermal insulation properties and hermetic sealing capabilities of galvanized steel drums especially valuable.
Six core engineering advantages that make galvanized steel drums the preferred choice for paint and coating manufacturers worldwide.
The zinc galvanisation layer provides a sacrificial barrier against rust and oxidation, critical when storing solvent-based paints, alkyd resins, and chemically aggressive coating formulations over extended periods.
Galvanized steel maintains structural integrity when exposed to a broad spectrum of coating chemistries including acrylics, epoxies, polyurethanes, and alkyd systems, preventing leaching or contamination of the stored product.
Heavy-gauge steel construction withstands the rigours of industrial handling, forklift operations, stacking, and long-distance freight — maintaining dimensional stability and seal integrity throughout the supply chain.
Precision-engineered flanges, lids, and closures ensure airtight containment that prevents solvent evaporation, moisture ingress, and cross-contamination — preserving coating viscosity and colour accuracy.
Steel is the world's most recycled material. Galvanized drums can be reconditioned and reused multiple times, and at end-of-life, they are 100% recyclable — supporting circular economy commitments in the coatings industry.
Our galvanized drums meet international standards including UN/DOT hazardous goods certifications, ISO quality frameworks, and regional compliance requirements for chemical packaging in the EU, Asia-Pacific, and Americas markets.
Understanding how galvanized chemical drums serve distinct roles across the paint and coating manufacturing value chain.
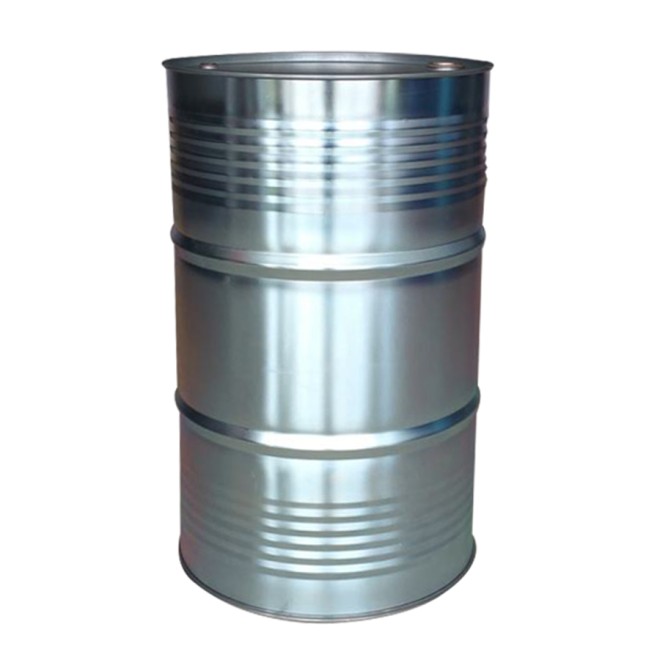
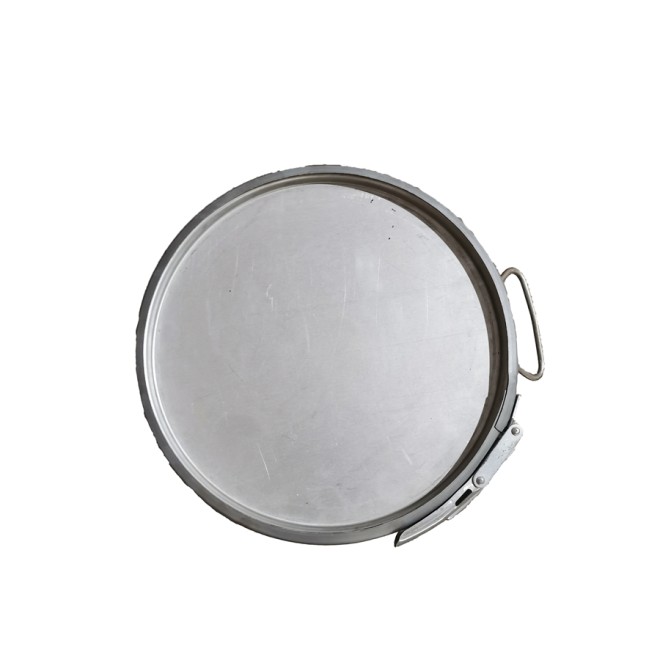
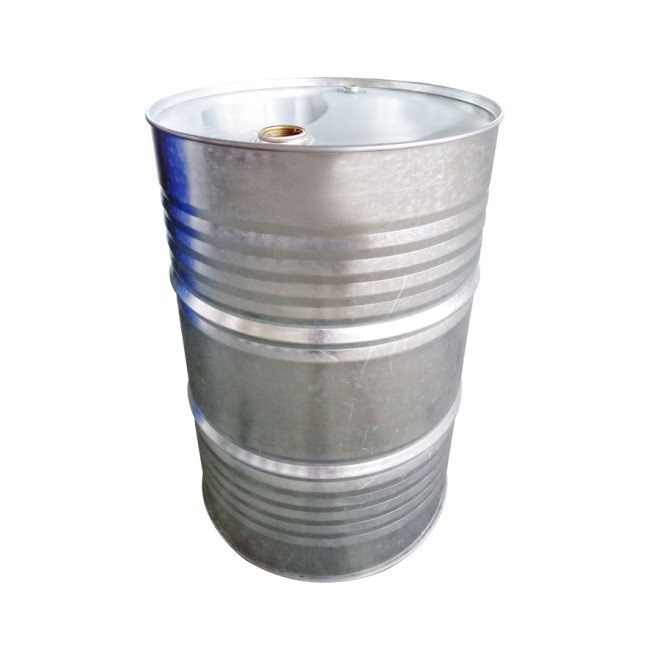
Large-format galvanized open-top drums (200–230L) are the workhorse of architectural paint manufacturing facilities, used for bulk storage of pigment pastes, binder emulsions, and finished coating products awaiting filling into retail containers. Their wide-mouth design facilitates easy mixing access and thorough drum cleaning between production batches.
The 70L large conical drum is specifically engineered for powder coating paint, where electrostatic properties and moisture exclusion are paramount. The conical geometry facilitates complete powder evacuation, minimising waste and simplifying the filling process in automated production lines.
Galvanized closed-top drums with single-flange construction are the standard for export shipments of industrial coatings, providing the structural rigidity and tamper-evident sealing required for compliance with international maritime and air freight regulations for hazardous chemicals.
Heavy-duty anti-corrosion coatings, marine paints, and industrial maintenance products require drums capable of withstanding harsh storage environments — offshore platforms, construction sites, and remote industrial facilities — where the galvanized steel's inherent weather resistance delivers unmatched performance.
Smaller-capacity stainless steel and galvanized drums (10L range) serve coating research laboratories and specialty formulation producers who require precise small-batch storage with the same chemical integrity guarantees as production-scale containers.
As the industry transitions to water-based, low-VOC, and bio-based coating systems, galvanized drums — particularly those with food-grade interior linings — provide the contamination-free environment these sensitive formulations require, preventing microbial growth and maintaining pH stability.
The galvanized drum manufacturing sector is evolving rapidly in response to shifting demands from paint and coating producers.
RFID and QR-code labelling systems are being integrated into drum designs, enabling coating manufacturers to implement full batch traceability, real-time inventory management, and automated quality control throughout the production and distribution cycle.
Advanced high-strength steel alloys and optimised drum geometry are enabling manufacturers to reduce drum tare weight by 8–15% without sacrificing structural performance — reducing freight costs and carbon footprint for coating exporters.
New-generation epoxy-phenolic and fluoropolymer interior lining technologies are expanding the chemical compatibility range of galvanized drums, enabling storage of highly reactive or pH-sensitive coating formulations that previously required costlier stainless steel containers.
Leading paint manufacturers are establishing closed-loop drum return and reconditioning programmes, with galvanized steel's inherent durability making it the ideal material for multi-cycle reuse — reducing packaging costs by up to 40% over a five-year horizon.
Rapid growth in African, South Asian, and Latin American coating markets is driving demand for region-specific drum configurations — including tapered-bottom designs for ease of transport on varied terrain and smaller-capacity formats suited to local distribution networks.
As coating manufacturers invest in automated filling, labelling, and palletising lines, drum designs are being optimised for robotic handling — with standardised flange dimensions, improved lid-removal mechanisms, and consistent dimensional tolerances that minimise line stoppages.
Established in 1999, the company was renamed Foshan Qiaoyue Packaging Co., Ltd. in 2007 (formerly known as Nanzhuang Ironworks Metal Products Factory). It stands as Foshan's sole manufacturer capable of producing diverse types of drum products.
Foshan Jinqi Barrel Manufacturing Co., Ltd. employs over 50 staff members and adheres to the principles of prioritising reputation, ensuring reliable quality, pursuing volume sales with modest profit margins, placing customers first, upholding ethical standards, protecting the environment, fostering innovation, and maintaining a spirit of continuous learning.
We are dedicated to providing our extensive clientele with high-quality, prompt, comprehensive services that prioritise customer requirements. Our company's conviction is to fulfil our social responsibilities to all stakeholders, including employees and customers, while pursuing sustainable business development.
Get Started Now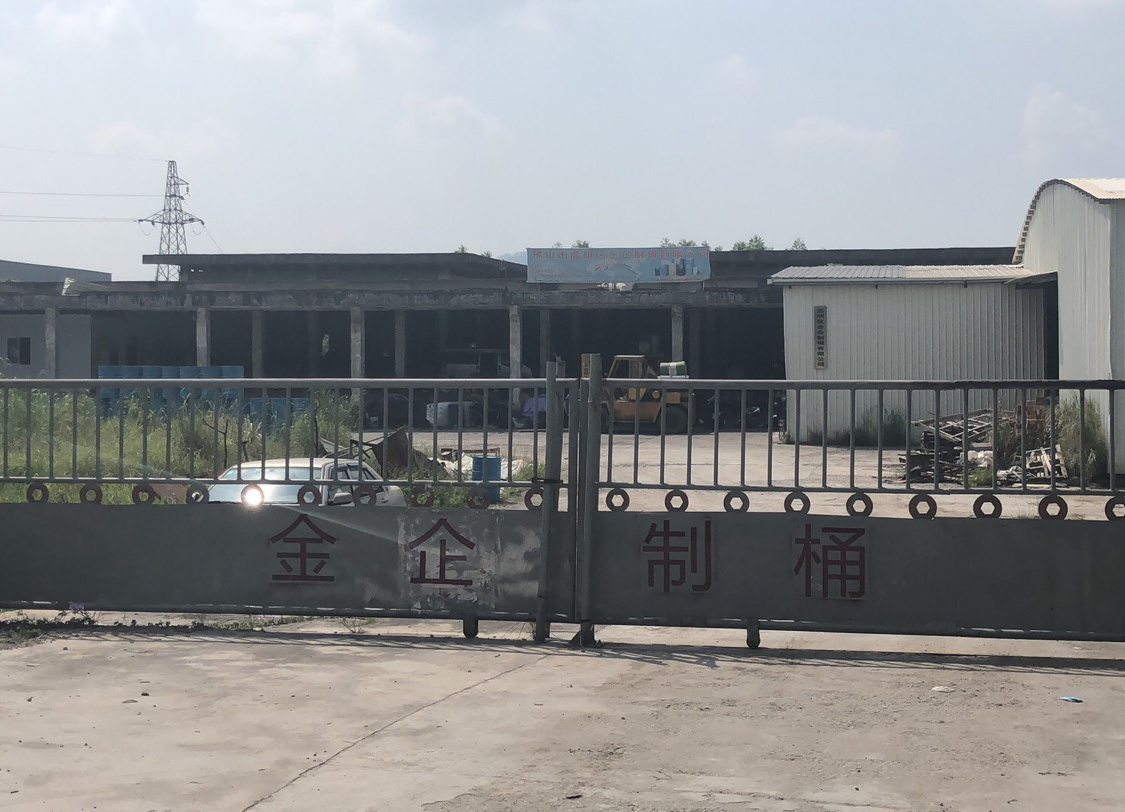
The values that have driven our growth and earned the trust of paint and coating manufacturers globally since 1999.

We pledge to deliver within agreed deadlines, meet specified standards, and stand by our commitment with our company's reputation as guarantee.

We strive to exceed customer expectations, producing products worthy of their trust.

We offer competitive pricing to serve our broad customer base.

We prioritise client requirements, tailoring our production to meet their specifications.
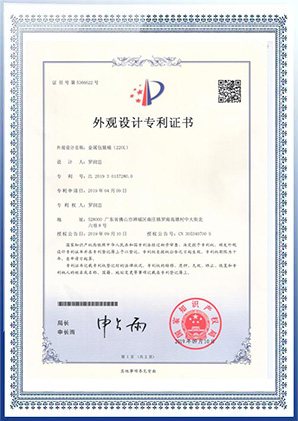
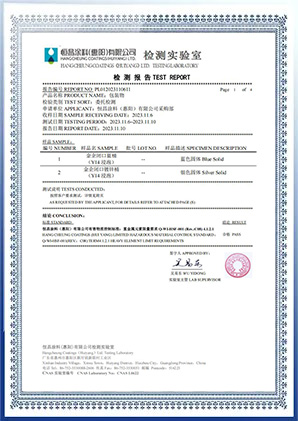
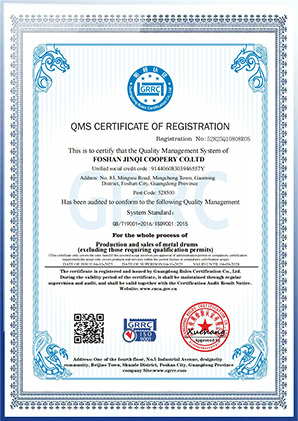
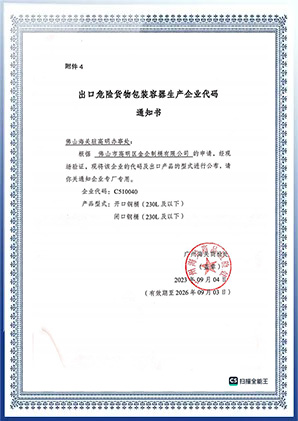
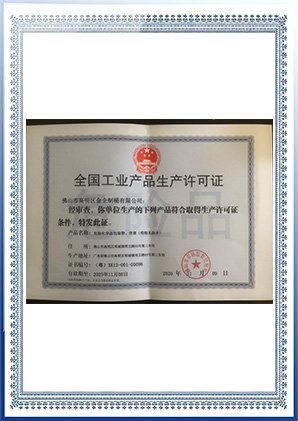
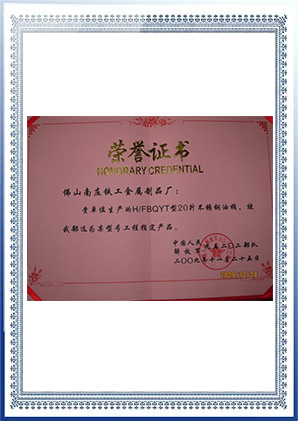
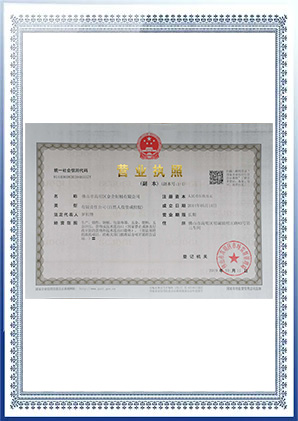
Our certifications reflect our commitment to quality, safety, and compliance in every galvanized drum we manufacture.
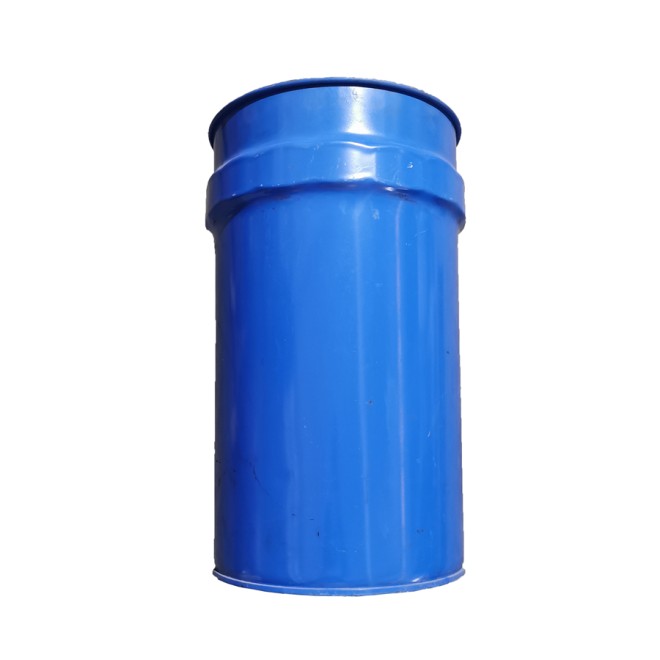
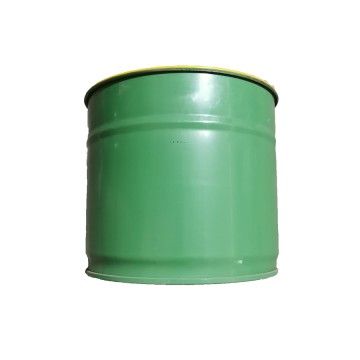
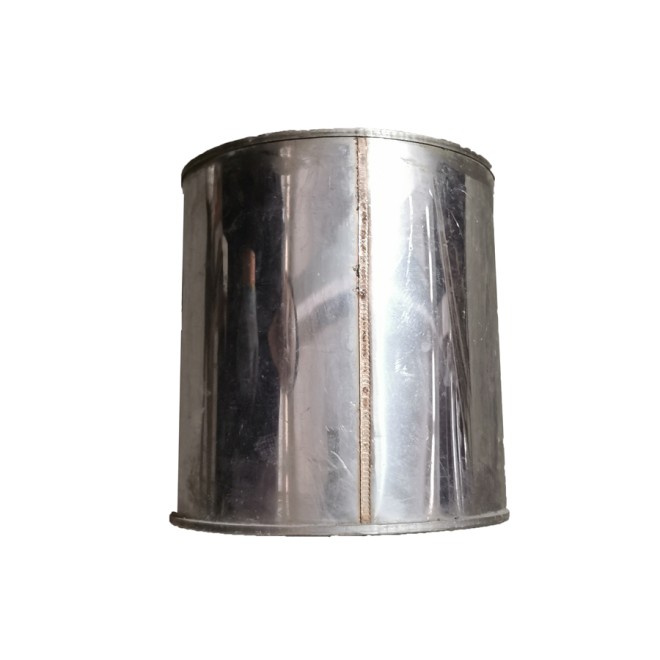
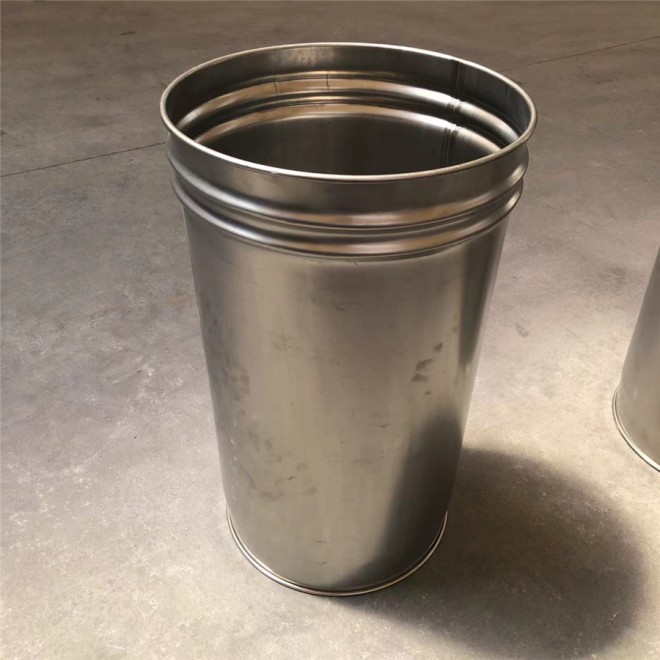
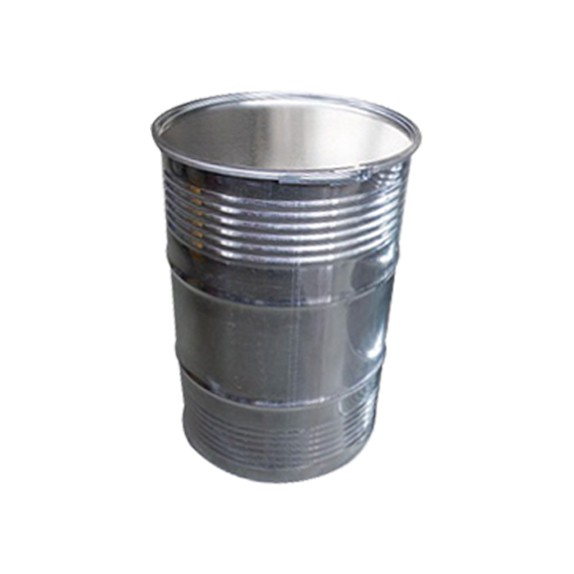
From compact 10L laboratory drums to industrial 200–230L bulk containers — our full product range covers every packaging need in the coatings manufacturing sector.
Whether you are scaling architectural coating production, optimising your powder coating supply chain, or seeking certified export-grade chemical drum solutions — our team is ready to deliver.
Get Started Now