

0102030405
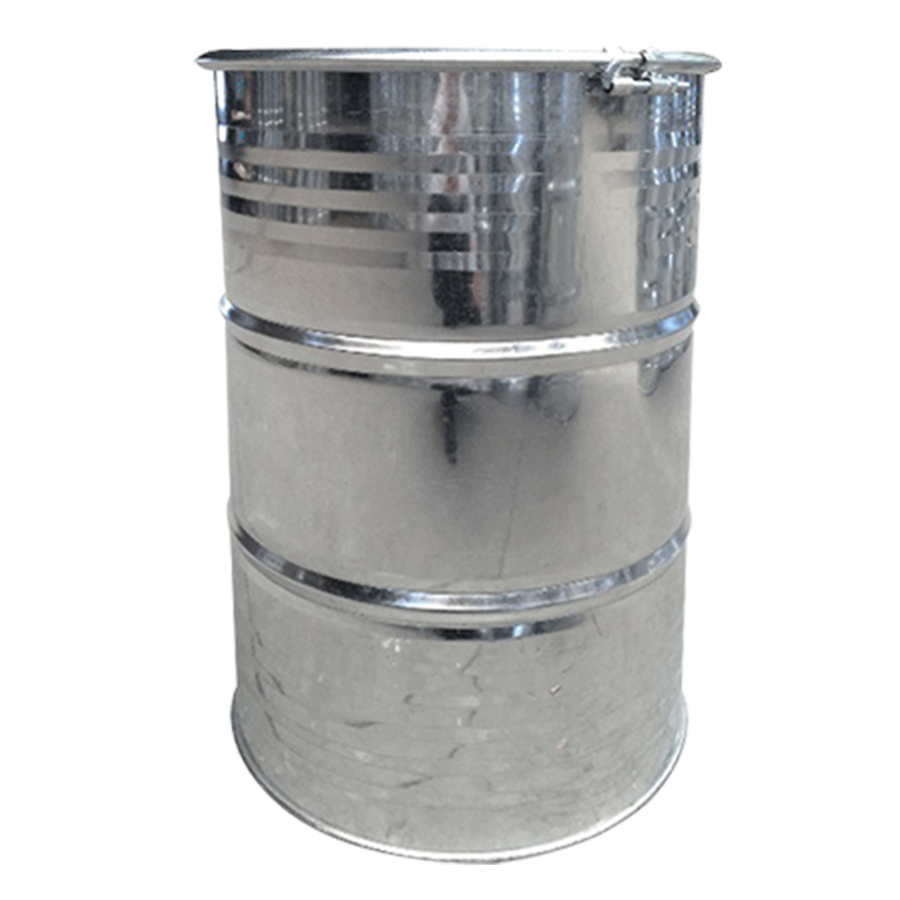
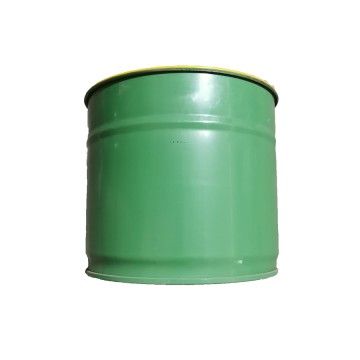
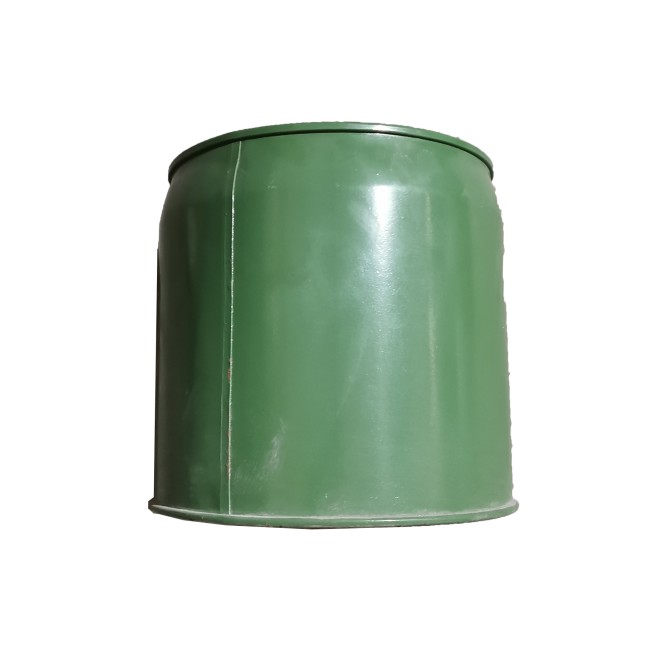
China Stainless Steel Conical Open-Top Drum 200–230L - Factory Direct Suppliers for Industrial Applications
🔩
Core Material: Food-grade stainless steel, built on a foundation of quality
The product body is crafted from 304/316L food-grade stainless steel, eliminating the inherent rust and corrosion issues common in standard steel from the outset. This stainless steel not only exhibits outstanding resistance to acids, alkalis, and oxidation, ensuring safe contact with corrosive liquids, food ingredients, and pharmaceutical intermediates, but also possesses excellent high-temperature tolerance. It operates seamlessly across a broad temperature range of -20°C to 120°C, effortlessly handling both low-temperature refrigerated storage and medium-temperature material handling. Furthermore, the stainless steel surface is smooth and dense, free from pores and impurities, making it resistant to bacterial growth. It complies with food hygiene and pharmaceutical GMP standards, facilitates easy cleaning, and is reusable, balancing practicality with environmental sustainability.
📐
Tapered Structure: Scientific Design Optimising Storage and Discharge
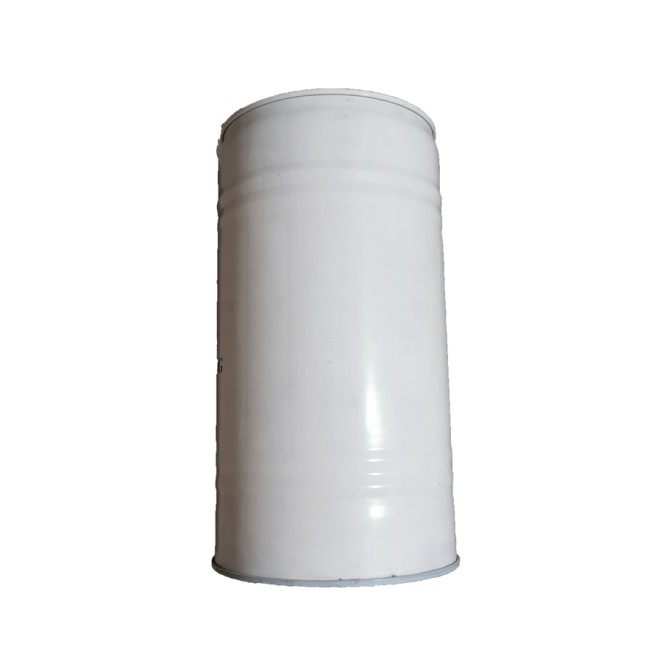
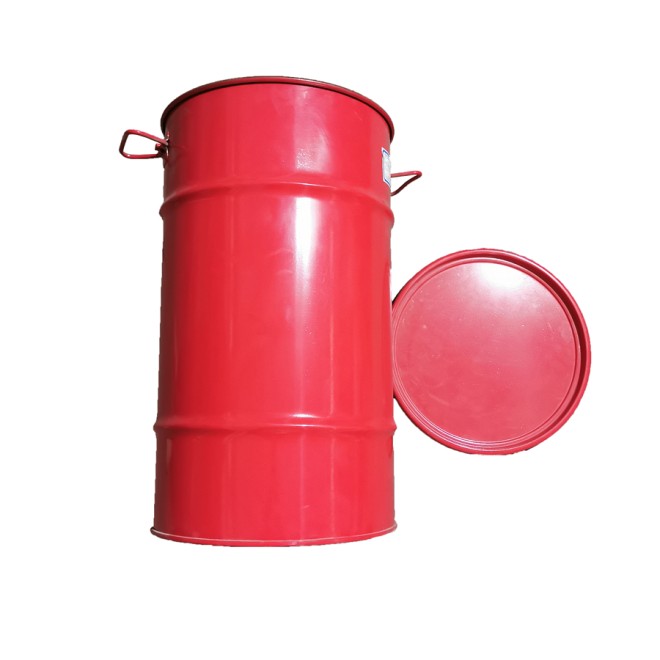
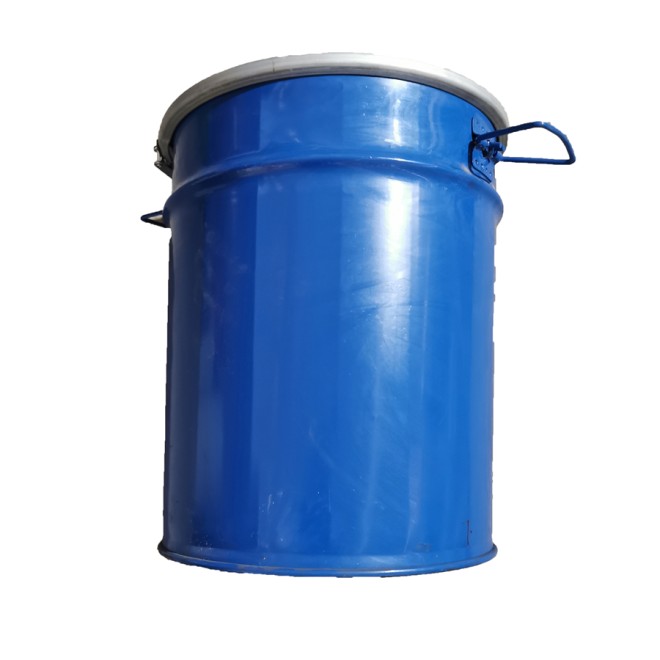
The product features a unique tapered structure, wider at the top and narrower at the bottom, offering multiple practical advantages over traditional cylindrical containers. The wide upper opening facilitates rapid filling of materials—be it granular, powdered, or liquid substances—enabling effortless pouring with minimal spillage. The tapered lower section, combined with a precision-engineered base interface, ensures thorough material discharge, effectively preventing residue waste. This makes it particularly suitable for storing and transferring high-value materials. The barrel's taper angle is mechanically optimised to guarantee structural stability while reducing overall weight. This facilitates effortless handling and stacking, with stacked containers forming stable support structures to save storage space.
⚙️
Craftsmanship Details: Meticulous Design for Safety and Convenience
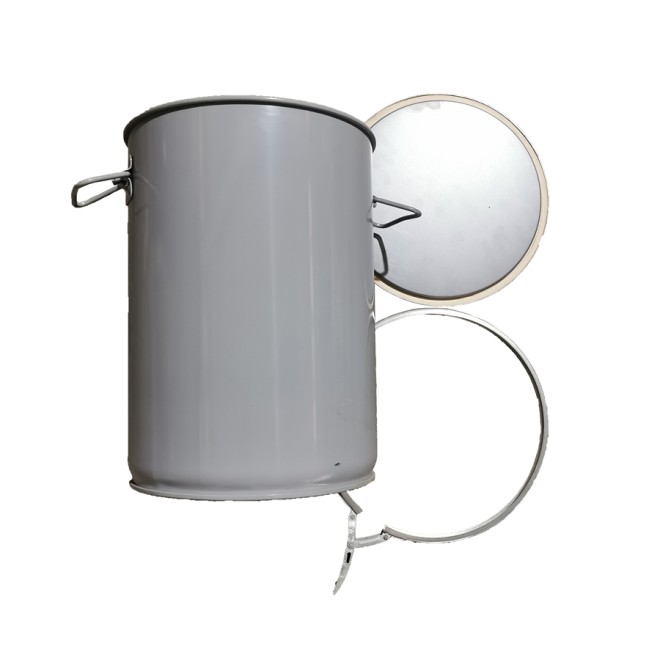
The standout opening design features a wide-diameter, flared rim structure paired with a removable dust cover. This facilitates frequent material retrieval and rapid filling while effectively blocking external dust and contaminants. The rim undergoes smooth polishing to eliminate sharp burrs, preventing hand injuries during handling or cleaning for enhanced safety.
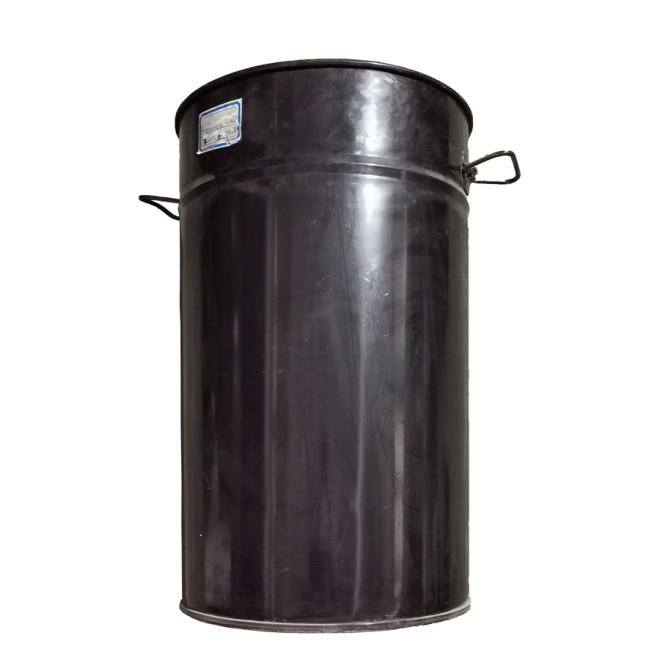
The barrel body employs an integrated stamping process, eliminating weld seams or utilising seamless welding technology. Welds are smooth and flat, matching the strength of the base material to completely eliminate leakage risks. Thoughtful reinforcements or anti-slip patterns are incorporated on the exterior. Handles, crafted from the same stainless steel as the barrel body, offer robust load-bearing capacity and comfortable, slip-resistant grip during transport. Certain models can be fitted with castors upon request, significantly enhancing mobility for diverse operational needs such as workshop batching or warehouse temporary storage.
🏭
Applications: Multi-sector compatibility with outstanding value
Boasting stable performance and user-friendly operation, this stainless steel conical open-top drum finds broad application across multiple sectors:
- 🍞 Food Industry: Temporary workshop storage for flour, grains, and semi-finished sauces, enabling convenient access and hygienic handling.
- 🧪 Chemical Industry: Handles neutral materials, solid particles, and non-volatile liquids safely and efficiently.
- 💊 Pharmaceutical Industry: Serves as a temporary container for non-sterile excipients, meeting GMP compliance requirements.
- 🔧 Machinery & Workshop: Provides open-top replenishment for workshop lubricants and coolants with ease.
- 📦 Warehouse & Logistics: Whether as a production mixing vessel, warehouse holding container, or maintenance supply bucket — its durability, convenience, and safety reduce operational costs while enhancing material retrieval efficiency.
❓
Frequently Asked Questions
Q
What grade of stainless steel is used in these conical open-top drums?
The drums are manufactured using 304 or 316L food-grade stainless steel. Both grades offer excellent corrosion resistance, while 316L provides enhanced protection against chlorides and acidic environments, making it ideal for more demanding pharmaceutical or chemical applications.
Q
What temperature range can these drums handle?
These stainless steel conical drums operate reliably across a wide temperature range of -20°C to 120°C, making them suitable for refrigerated cold storage environments as well as medium-temperature processing and material handling tasks.
Q
Are these drums compliant with food and pharmaceutical hygiene standards?
Yes. The smooth, pore-free stainless steel surface resists bacterial growth and is easy to clean. These drums comply with food hygiene regulations and pharmaceutical GMP standards, making them suitable for use in food processing, pharmaceutical production, and other regulated industries.
Q
What is the advantage of the tapered design compared to cylindrical containers?
The tapered design — wider at the top and narrower at the bottom — offers several key benefits: it allows faster filling with less spillage, ensures complete material discharge to minimise waste, and enables stable stacking to save storage space. The optimised taper angle also reduces overall weight for easier handling.
Q
Can castors or wheels be added to the drum for easier movement?
Yes. Certain models can be fitted with castors upon request, significantly improving mobility for applications such as workshop batching, production line operations, or warehouse material handling where frequent repositioning is required.
Q
What industries are these stainless steel conical drums best suited for?
These drums are highly versatile and widely used across multiple sectors including food processing, chemical handling, pharmaceutical manufacturing, machinery maintenance, and general warehouse storage. They function effectively as mixing vessels, temporary holding containers, or maintenance supply buckets, reducing operational costs while improving efficiency.