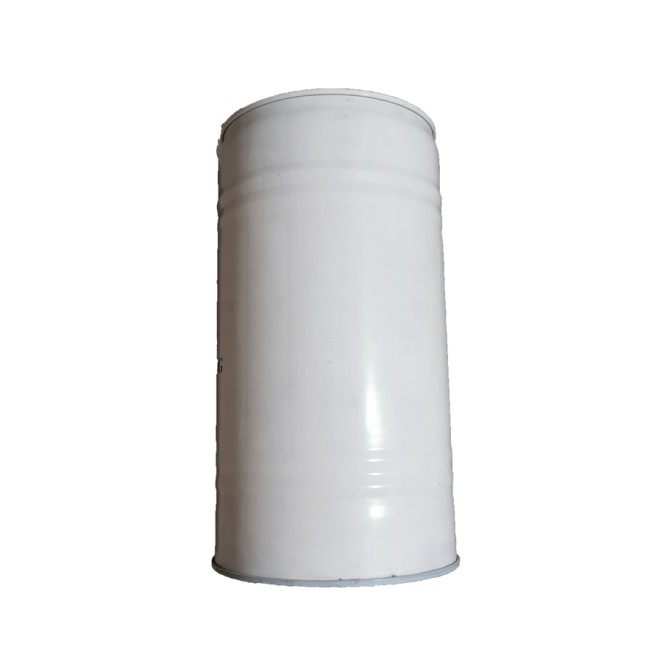
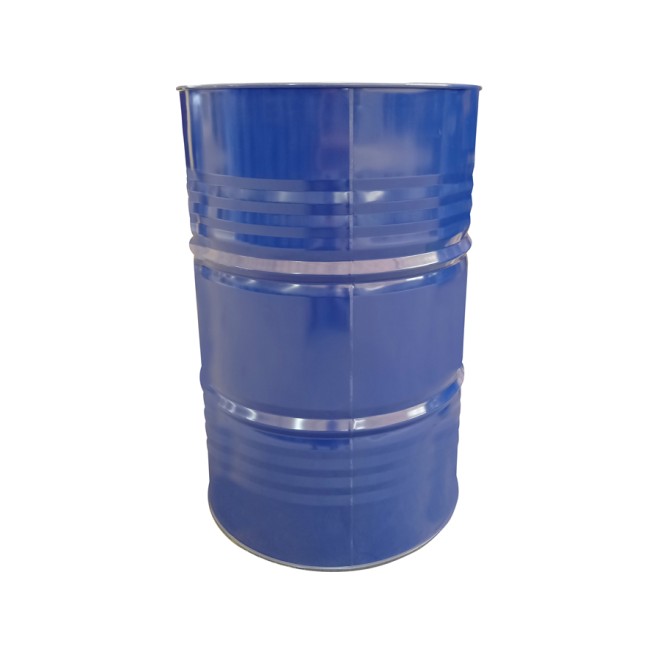
China Stainless Steel Conical Closed-Top Drum - Durable Storage Solutions from Trusted Suppliers and Factory
,
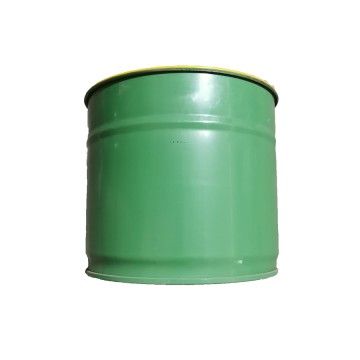
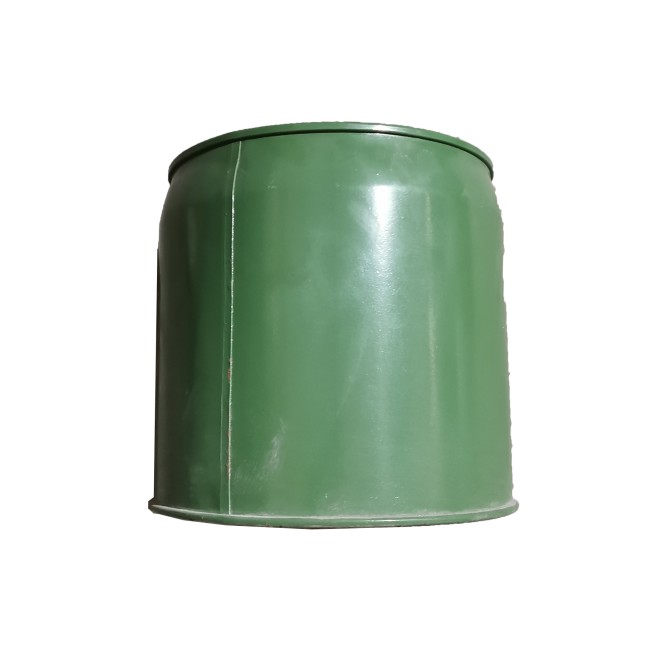
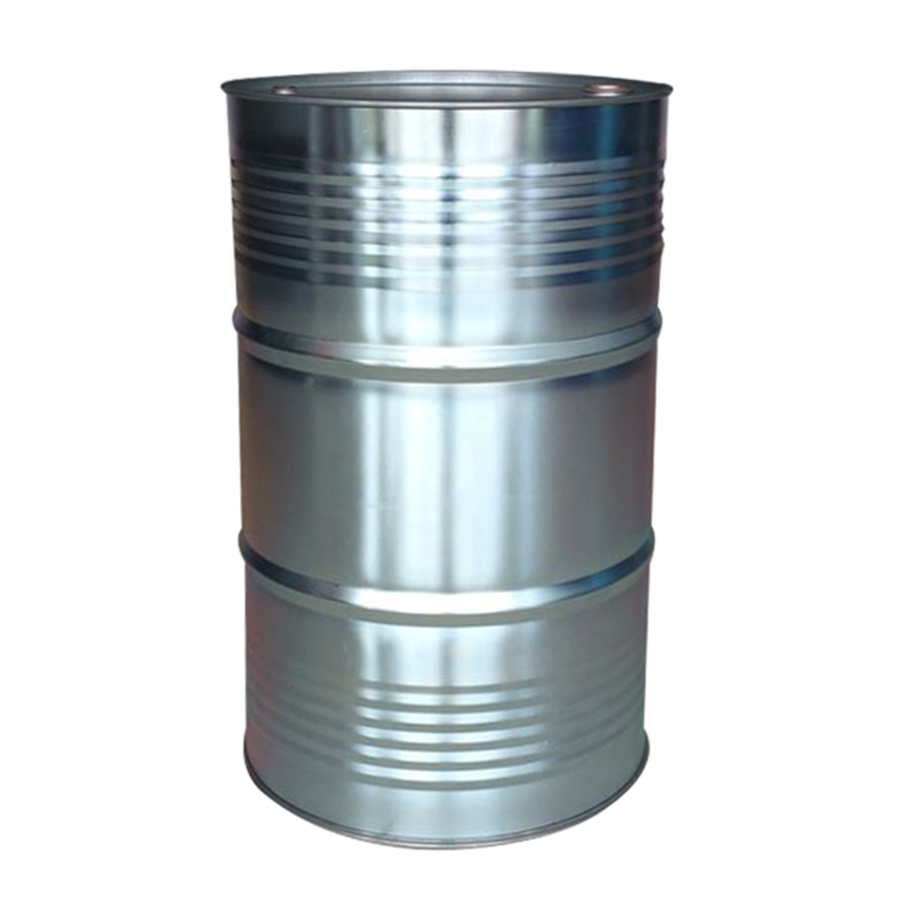
Discover our premium stainless steel conical closed-top drum, designed specifically for industrial storage, logistics transport, and specialized applications. Manufactured by leading China suppliers, this sealed container boasts superior material properties and a scientifically engineered conical structure. With an advanced closed-top sealing system, it is the perfect solution for various sectors such as chemicals, foodstuffs, pharmaceuticals, and machinery. Our factory strictly adheres to industry standards throughout every stage, from raw material selection to the manufacturing process, ensuring exceptional durability, sealing integrity, and safety for all your storage needs.
Core Material: Food-Grade Stainless Steel, Built on a Foundation of Quality
The product body is crafted from 304/316L food-grade stainless steel, eliminating the inherent rust and corrosion issues common in standard steel from the outset. This stainless steel not only exhibits outstanding resistance to acids, alkalis, and oxidation, ensuring safe contact with corrosive liquids, food ingredients, and pharmaceutical intermediates, but also possesses excellent high-temperature tolerance.
✅ Operates seamlessly across a broad temperature range of -20°C to 120°C, effortlessly handling both low-temperature refrigerated storage and medium-temperature material handling.
Furthermore, the stainless steel surface is smooth and dense, free from pores and impurities, making it resistant to bacterial growth. It complies with food hygiene and pharmaceutical GMP standards, facilitates easy cleaning, and is reusable, balancing practicality with environmental sustainability.
Tapered Structure: Scientific Design Optimising Storage and Discharge
The product features a distinctive tapered structure — wider at the top and narrower at the bottom — offering multiple practical advantages over traditional cylindrical containers.
🔹 The wide upper opening facilitates rapid filling of materials — be they granular, powdered, or liquid — minimising spillage and waste.
🔹 The narrow conical base, combined with a precision-engineered bottom interface, ensures thorough discharge of contents, effectively preventing residue waste. This design is particularly suited for the storage and transfer of high-value materials.
The barrel's taper angle is mechanically optimised to ensure structural stability while reducing overall weight. This facilitates effortless handling and stacking, with stacked containers providing stable support to save storage space.
Zero Residue Discharge
Space-Saving Stacking
Lightweight Design
Craftsmanship Details: Meticulous Design Balancing Safety and Convenience
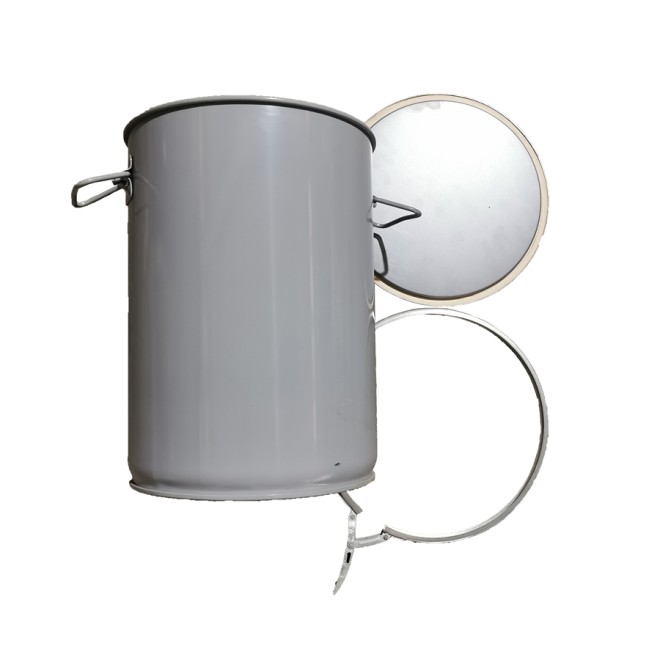
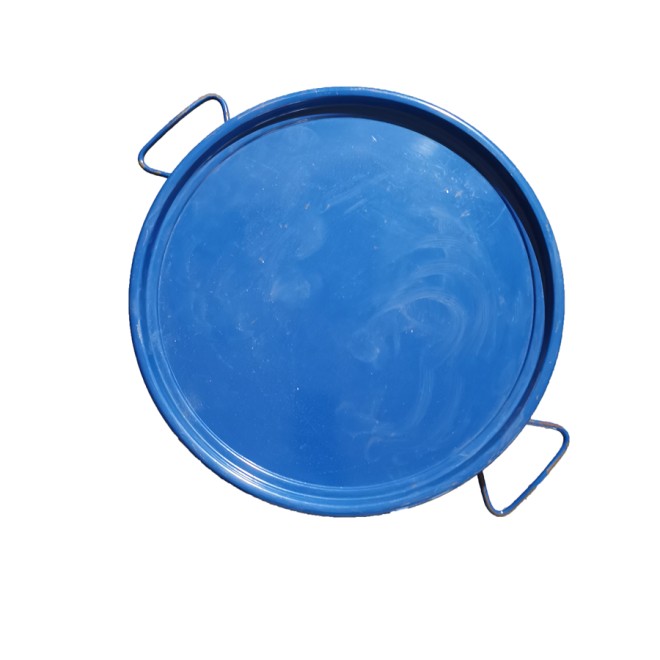
🔒 Sealing Performance: The closed-top design employs an integrated sealing structure with dual sealing grooves and an internal food-grade silicone seal ring. Combined with anti-theft threaded locking technology, it withstands 0.1MPa sealing pressure — effectively preventing liquid leakage, gas volatilisation, and external contaminant ingress.
This makes it particularly suitable for storing and transporting flammable, explosive, volatile, or high-purity materials. The drum body employs an integrated stamping process — either seamless or featuring seamless welding technology. Weld seams are smooth and flat, matching the strength of the base material, completely eliminating the risk of leakage.
🖐️ Ergonomic Handling: The exterior features thoughtfully designed reinforced handles or anti-slip texturing. Handles are crafted from the same stainless steel as the drum body, offering robust load-bearing capacity and comfortable, slip-resistant grip. Select models can be fitted with castors upon request, significantly enhancing mobility across workshops and warehouses.
0.1MPa Seal Tested
Seamless Welding
Optional Castor Wheels
Anti-Theft Lock
Applications: Multi-Sector Compatibility with Outstanding Value
Boasting stable performance and superior sealing, this stainless steel conical closed-top drum serves diverse industries:
Chemical Industry: Transfers neutral/mildly corrosive liquids, volatile solvents, and chemical additives.
Pharmaceuticals: Sealed storage vessel for medicinal intermediates and sterile excipients.
Machinery: Holds precision materials like lubricants and coolants.
Whether deployed as a production-stage transfer drum, a sealed storage container for warehousing, or a secure transport vessel for logistics — its durability, sealing integrity, and portability reduce operational costs while enhancing efficiency and material safety.
Frequently Asked Questions
Q1
What is the difference between 304 and 316L stainless steel, and which should I choose?
Both 304 and 316L are food-grade stainless steels, but 316L contains added molybdenum, which provides superior resistance to chloride corrosion and stronger acids. If your application involves highly corrosive chemicals, saltwater environments, or pharmaceutical-grade purity requirements, 316L is the recommended choice. For general food, beverage, or light chemical use, 304 offers excellent performance at a more cost-effective price point.
Q2
What is the maximum operating temperature for these stainless steel conical drums?
The drums are engineered to operate across a broad temperature range of -20°C to 120°C. This makes them suitable for both refrigerated cold storage environments and medium-temperature material handling processes, such as warm liquid transfer in food processing or pharmaceutical production.
Q3
How does the sealing system work, and what pressure can it withstand?
The drum features an integrated closed-top sealing structure with dual sealing grooves and an internal food-grade silicone seal ring. The anti-theft threaded locking mechanism creates a seamless contact seal upon tightening, rated to withstand 0.1MPa of sealing pressure. This effectively prevents liquid leakage, gas volatilisation, and contamination ingress — ideal for volatile, flammable, or high-purity materials.
Q4
Can the drums be stacked for storage, and are they stable when stacked?
Yes. The tapered conical design is specifically engineered to allow safe stacking. The mechanically optimised taper angle ensures that stacked drums interlock in a stable configuration, distributing weight evenly. This allows efficient use of vertical warehouse or storage space without compromising structural integrity or safety.
Q5
Are castor wheels available, and can they be added to existing drums?
Select models can be configured with castor wheels upon request at the time of ordering. Castors significantly enhance mobility, making it easy to manoeuvre the drums across workshop floors, production lines, and warehouse environments without manual lifting. Please contact us to confirm castor compatibility with your chosen drum model and capacity.
Q6
Do these drums comply with food safety and pharmaceutical GMP standards?
Yes. The food-grade stainless steel surface is smooth, dense, and free from pores or impurities, making it inherently resistant to bacterial growth and easy to clean thoroughly. The drums are designed to comply with international food hygiene regulations and pharmaceutical GMP (Good Manufacturing Practice) standards, making them a trusted choice for food processing, beverage production, and pharmaceutical manufacturing environments.